A pinhole steam leak hissing behind a pipe lagging in a power plant rarely gets noticed during a normal walkdown — it's too quiet to hear over the ambient plant noise and too small to see unless someone happens to look at exactly the right angle. Yet a single half-inch steam leak at typical plant pressure can waste enough energy in a year to cost tens of thousands of dollars, and that's before counting the safety risk of a technician walking past an invisible high-pressure jet. Acoustic AI sensors catch what the human ear and eye miss, flagging leaks inside OxMaint long before the next scheduled steam trap survey.
Steam System Efficiency
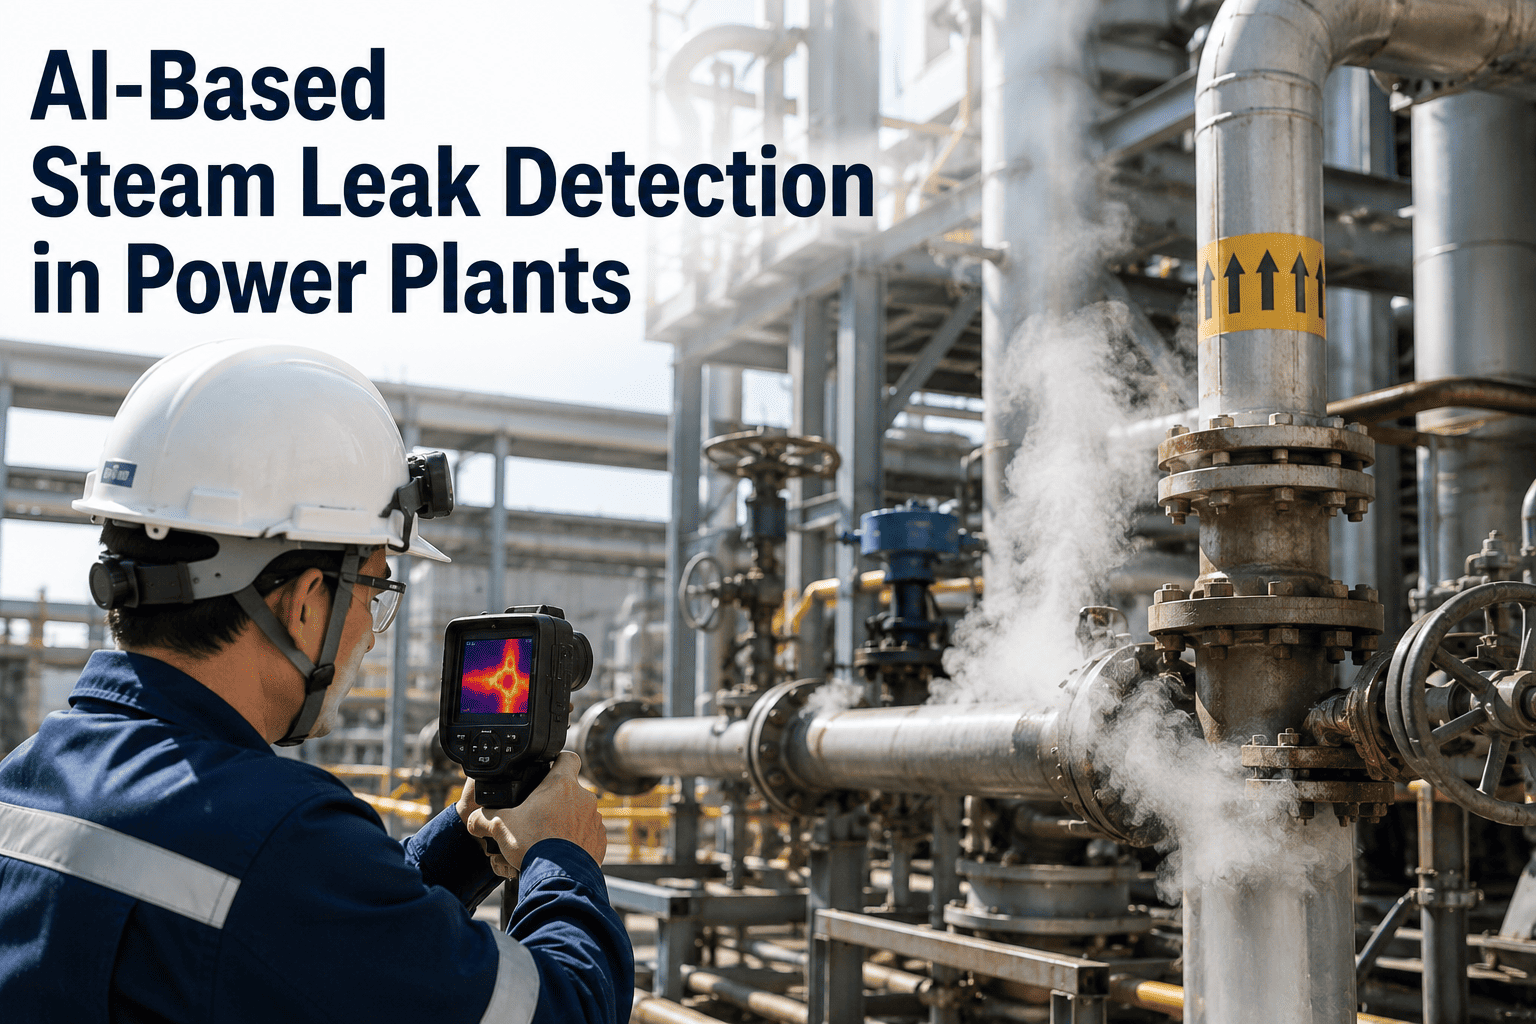
AI-Based Steam Leak Detection in Power Plants
Steam leaks waste energy continuously from the moment they start, and most go undetected for months between manual surveys. Acoustic sensors and AI pattern recognition catch the leak signature in days, not at the next quarterly walkdown.
What a steam leak actually costs over time
1/8 inch
~$4,000/year
at typical industrial steam pressure
1/4 inch
~$16,000/year
energy wasted continuously, undetected
1/2 inch
~$64,000/year
plus rising safety exposure on walkdowns
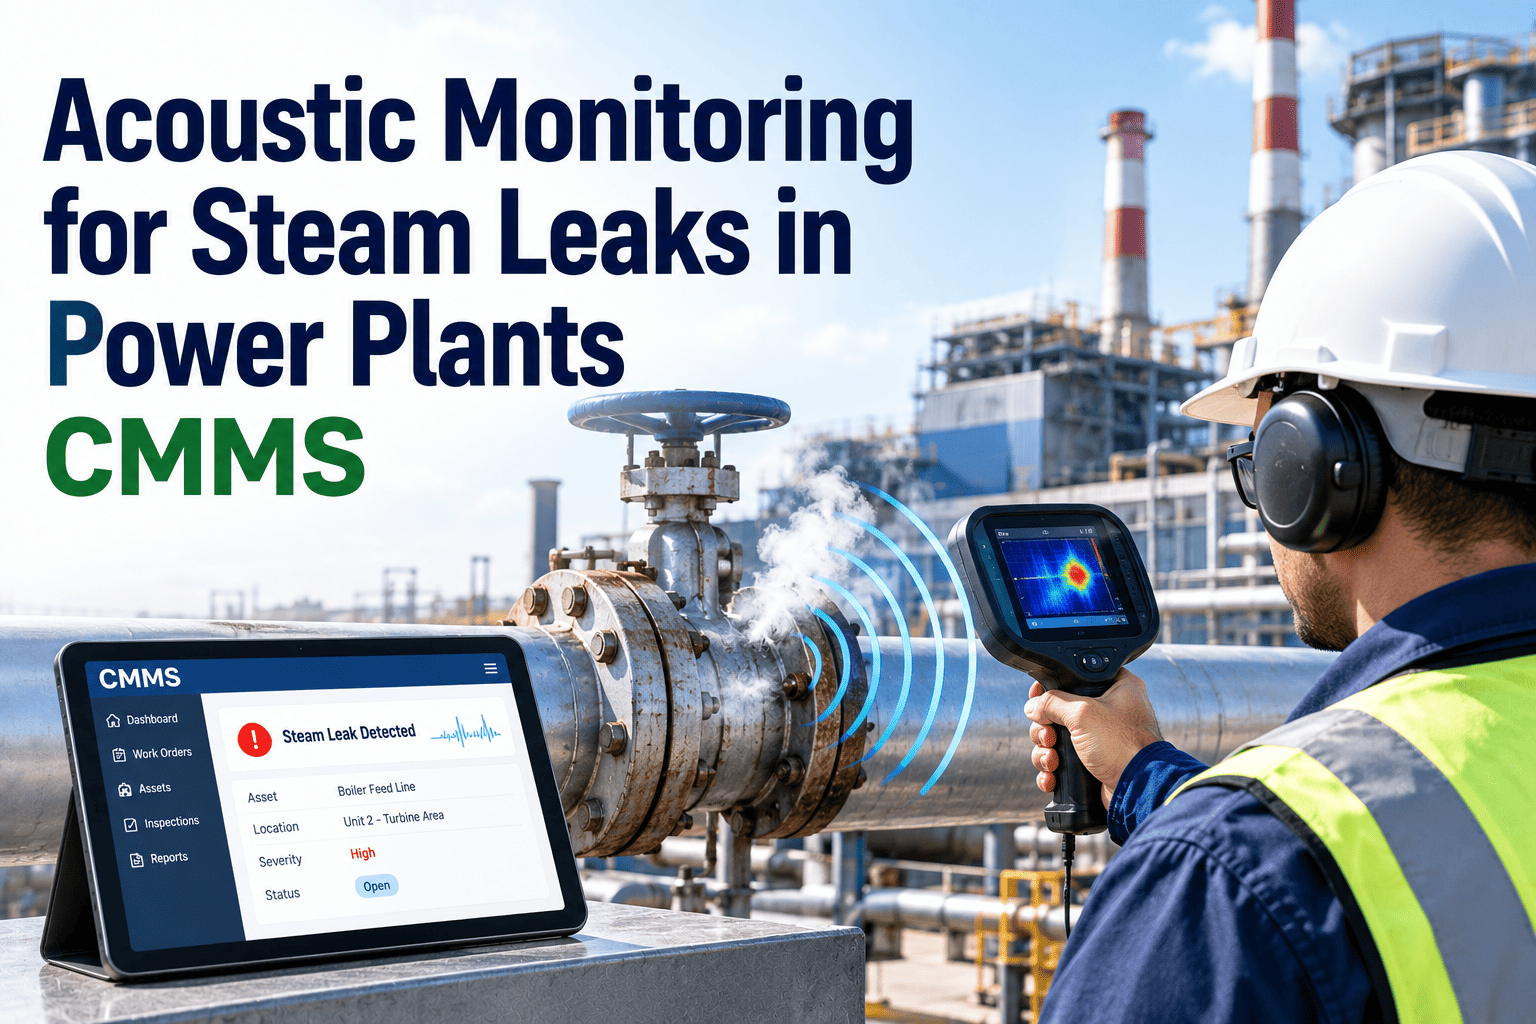
How acoustic detection finds what surveys miss
1
Acoustic sensors mounted along steam lines capture ultrasonic frequencies continuously
2
AI models distinguish leak signatures from normal flow noise and ambient plant sound
3
A flagged leak is pinpointed to a specific pipe section or trap, not a general area
4
A work order is generated automatically with estimated leak size and energy cost
Find out what your steam system is leaking right now
Bring your last steam trap survey results and we'll show what continuous monitoring would catch between surveys.
Quarterly survey versus continuous monitoring
| Factor | Quarterly Manual Survey | Continuous Acoustic Monitoring |
|---|
| Detection delay | Up to 90 days | Hours to a few days |
| Small leak sensitivity | Often missed by ear | Captures ultrasonic signatures |
| Coverage | Limited to accessible areas | Fixed and route-based sensors |
| Safety exposure | Technician near live steam lines | Remote monitoring, fewer walkdowns |
Where steam leaks most commonly originate
A
Failed-open steam traps that continue passing live steam after cycling stops working
B
Worn valve packing and gland seals around isolation and control valves
C
Pinhole corrosion at pipe joints and welds in older steam distribution runs
D
Damaged or missing insulation lagging that masks a leak's heat signature
How leak detection fits into a broader energy program
Steam leak detection rarely runs in isolation — most plants pair it with insulation surveys and trap maintenance programs so the energy savings compound across the whole steam distribution network rather than one fixed line at a time.
Phase 1
High-cost lines
Sensors on the steam lines with the highest pressure and flow first
Phase 2
Trap fleet
Continuous trap monitoring layered on top of fixed line sensors
Phase 3
Full network
Route-based scanning extends coverage to remaining distribution areas
Frequently asked questions
How does acoustic detection tell a leak apart from normal steam flow noise?
Steam leaks produce a distinct high-frequency ultrasonic signature caused by turbulent flow through a small opening, which differs from the lower-frequency sound of normal flow through pipe and valves. AI models trained on this signature filter out background plant noise and flag only the patterns consistent with an actual leak. This reduces false alarms compared to a basic decibel-threshold sensor. See how detection works inside
OxMaint.
Can this detect leaks from failed steam traps specifically?
Yes — a failed-open steam trap produces a continuous flow signature distinct from its normal cycling pattern, and the system flags traps that deviate from expected behavior over time. This is particularly valuable since trap failures are one of the largest sources of ongoing steam loss in most plants and are easy to miss during infrequent surveys. Each trap can be tracked individually on its own baseline.
Discuss trap monitoring on a call.
How many sensors does a typical steam system need?
Sensor count depends on steam line length, number of traps, and plant layout, with most installations using a mix of fixed sensors on high-risk lines and route-based handheld scanning for less critical areas. A phased rollout starting with the highest-pressure or highest-cost lines is common rather than instrumenting the entire system at once. This keeps initial investment focused on the areas with the fastest payback. Explore a coverage plan inside
OxMaint.
What's the typical payback period for steam leak detection?
Most plants recover the cost of sensor deployment within six to twelve months, primarily through avoided energy waste from leaks that would otherwise have gone undetected for one or more quarterly survey cycles. Plants with aging steam infrastructure or a history of multiple undetected leaks per year tend to see faster payback. The energy savings compound with every additional leak caught early rather than left running.
Get a payback estimate for your plant.
Does this replace the need for periodic manual steam trap surveys?
Continuous monitoring significantly reduces reliance on frequent manual surveys but most plants still run an annual physical inspection to verify sensor coverage and check areas without fixed instrumentation. The combination catches more leaks than either approach alone, since acoustic monitoring covers continuous time gaps while physical inspection verifies sensor accuracy and mechanical condition. This layered approach is what most plants settle on. Get started with
OxMaint today.
Stop paying for steam nobody can hear escaping
Get acoustic leak detection running on your highest-cost steam lines before the next survey cycle.