Overall Equipment Effectiveness (OEE) is the gold standard metric for measuring manufacturing productivity — and in food production, where margins are tight and compliance demands are constant, OEE optimization separates high-performing operations from chronically underperforming ones. If your food production line is running below the 85% world-class OEE benchmark, you are leaving measurable output, profitability, and competitive advantage on the table every single shift. This guide breaks down the practical strategies, CMMS data tools, and loss analysis frameworks that operations managers are using right now to drive sustainable OEE improvement in food manufacturing environments.
Start Tracking OEE Across Your Food Production Lines
OxMaint helps food manufacturers capture real-time availability, performance, and quality data — automatically calculating OEE by line, shift, and product SKU with zero manual spreadsheet work.
What Is OEE and Why Does It Matter for Food Manufacturing?
Overall Equipment Effectiveness is a composite metric that multiplies three factors — Availability, Performance, and Quality — to produce a single percentage that reflects how effectively a production asset is being utilized relative to its full potential. An OEE score of 100% means your equipment ran during all planned production time, at full rated speed, producing zero defects. In food manufacturing, where equipment downtime triggers product holds, where speed losses drive labor inefficiency, and where quality failures mean costly rework or disposal, each of the three OEE components maps directly to bottom-line impact.
The food and beverage industry typically operates with OEE scores between 55% and 65% — well below the 85% world-class benchmark. This gap represents an enormous opportunity. A packaging line running at 60% OEE that improves to 75% OEE adds the equivalent of 15% more production capacity without capital investment. Understanding where that gap lives — in unplanned downtime, speed losses, or quality failures — is the starting point for any meaningful OEE improvement program.
The Three OEE Components in Food Production Context
Availability
How much of planned production time is the line actually running?
- Unplanned equipment breakdowns
- Sanitation overruns between runs
- Allergen changeover delays
- Ingredient or material shortages
Performance
How fast is the line running vs. its rated design speed?
- Operators deliberately slowing lines
- Minor stops under 5 min (unreported)
- Upstream or downstream bottlenecks
- Product jams and sensor false triggers
Quality
What percentage of output passes first-time — no rework, no disposal?
- Checkweigher and fill weight rejects
- Metal detection or X-ray failures
- Cook temperature excursion disposals
- Startup rejects after each changeover
OEE Benchmarks for Food and Beverage Manufacturing
Understanding where your OEE scores stand relative to industry benchmarks is essential context for prioritizing improvement investment. Food production OEE benchmarks vary significantly by equipment type, product category, and operational complexity.
| Equipment / Process Type | Typical OEE Range | World-Class Target | Primary Loss Driver |
|---|---|---|---|
| High-Speed Packaging Lines | 55% – 68% | 82% – 85% | Minor stops and changeover |
| Filling and Portioning Equipment | 60% – 72% | 83% – 87% | Speed loss and startup rejects |
| Thermal Processing (Retorts, Ovens) | 70% – 80% | 88% – 92% | Unplanned downtime and quality |
| Dairy Processing Lines | 58% – 70% | 80% – 85% | Sanitation time and changeover |
| Meat and Poultry Processing | 55% – 65% | 78% – 82% | Availability and quality losses |
| Beverage Filling Lines | 62% – 74% | 84% – 88% | Minor stops and performance |
| Bakery and Snack Production | 60% – 70% | 82% – 86% | Changeover and startup rejects |
These benchmarks reveal that no food production environment is immune to OEE loss, and that the loss categories differ meaningfully by equipment type. Targeting OEE improvement without first identifying which of the three components is the primary drag produces unfocused action plans. A filling line with 78% availability, 91% performance, and 89% quality has a fundamentally different improvement path than a packaging line with 90% availability, 74% performance, and 88% quality — even if both lines arrive at a similar composite OEE score.
The Six Big Losses in Food Production — and How to Attack Each One
The Six Big Losses framework — developed within the Total Productive Maintenance methodology — categorizes every OEE loss into one of six types, each mapping to one of the three OEE components. For food manufacturing operations managers, this framework provides the analytical structure needed to move from "our OEE is too low" to "here is exactly where and why we are losing OEE, and here is what we are doing about it."
Equipment Failure & Unplanned Downtime
Every unplanned breakdown pulls maintenance into firefighting mode — costing production time, labor, and schedule recovery.
- Aging or unmaintained equipment
- No predictive maintenance program
- Reactive-only maintenance culture
- CMMS-driven preventive maintenance schedules
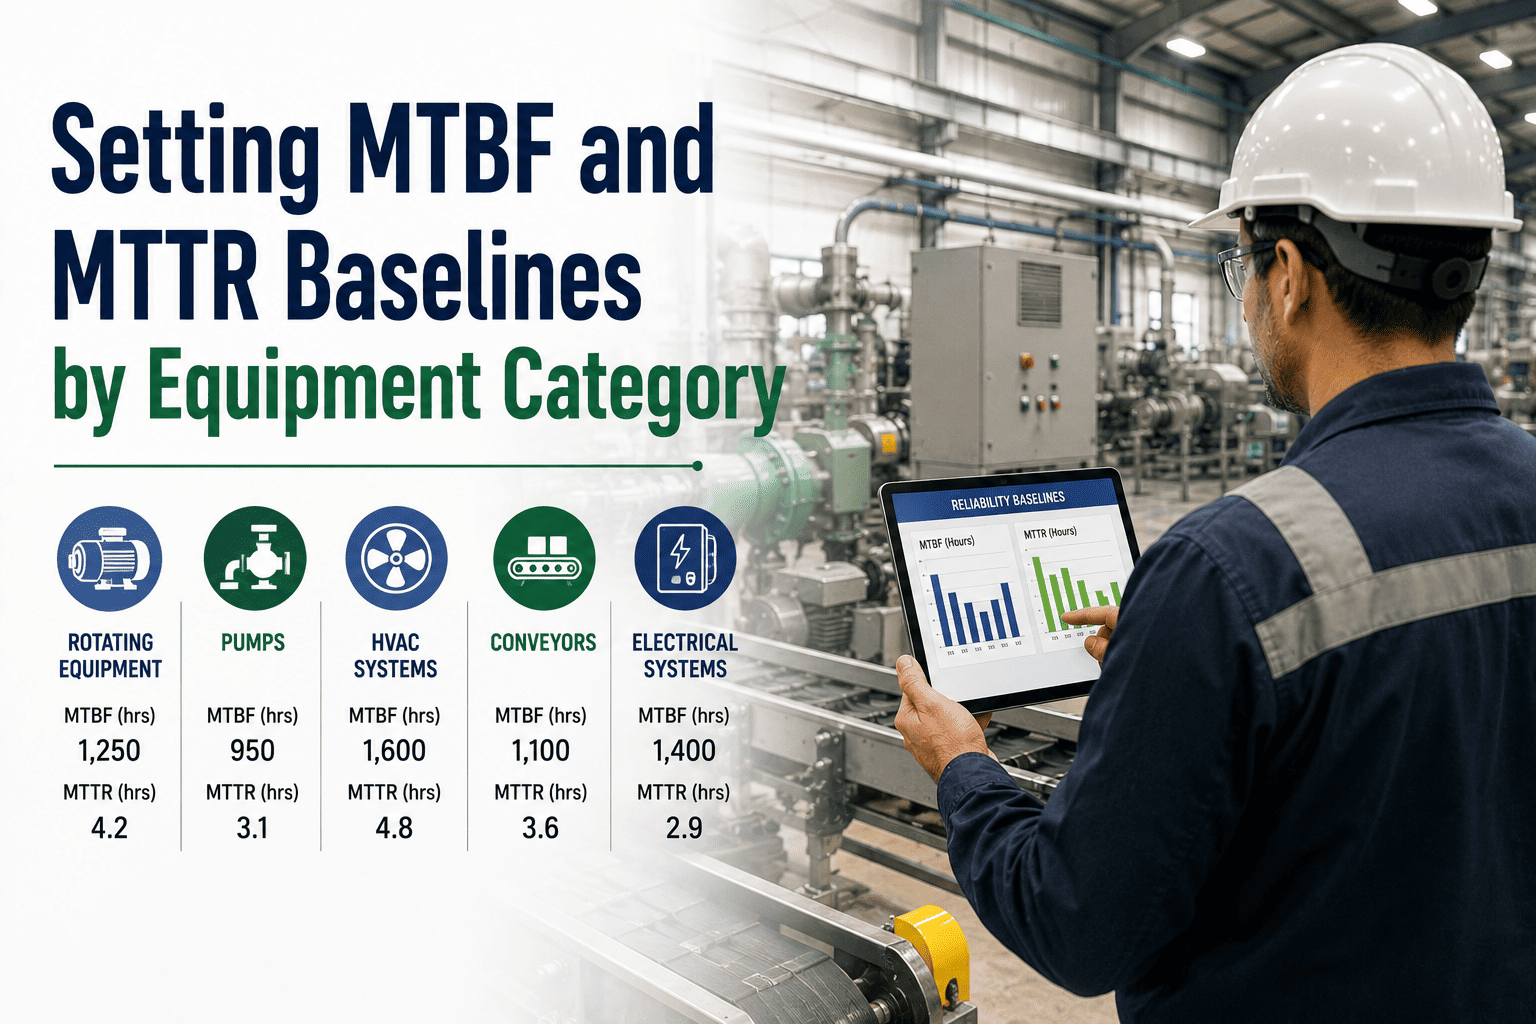
- MTBF analysis by equipment and failure mode
- Sensor-based predictive monitoring
Setup and Changeover Losses
Changeovers in food plants combine mechanical setup with mandatory sanitation — any overrun recurs every single product transition.
- Allergen sanitation overruns
- No standardised changeover procedure
- Parts or tools not pre-staged
- SMED — move tasks external to line stop
- CMMS actual vs. planned changeover tracking
- Pre-staged kits and visual SOP boards
Idling and Minor Stops
Stops under 5 min never make the downtime report — but 40 minor stops × 3 min each = 2 hours of silent lost production per shift.
- Label misfeeds and product jams
- Sealing inconsistencies on packaging lines
- Sensor false triggers
- Automated stop event capture (all durations)
- Pareto analysis of minor stop causes
- Operator-led quick-fix kaizen events
Reduced Speed Operation
Running below rated speed feels like a safe choice — but it's an invisible, continuous performance loss that rarely gets questioned.
- Variable-viscosity product handling
- Upstream feed inconsistency
- Film or packaging format limitations
- OEE performance tracking vs. rated speed
- Raw material spec tightening
- Equipment adjustment and revalidation
Startup and Changeover Rejects
Product made while the line stabilises after startup doesn't pass spec — and in high-changeover operations, this adds up fast.
- Fill weight instability at startup
- Temperature not yet at target
- No standard startup sequence
- Standardised startup checklists in CMMS
- Track time-to-stability per run
- Reduce changeover frequency via run scheduling
Production Rejects and Rework
In-process rejects hit OEE directly and carry extra risk in food — non-conforming product may also trigger HACCP corrective action.
- Checkweigher and fill deviation failures
- Metal detection or X-ray rejects
- Process drift during long runs
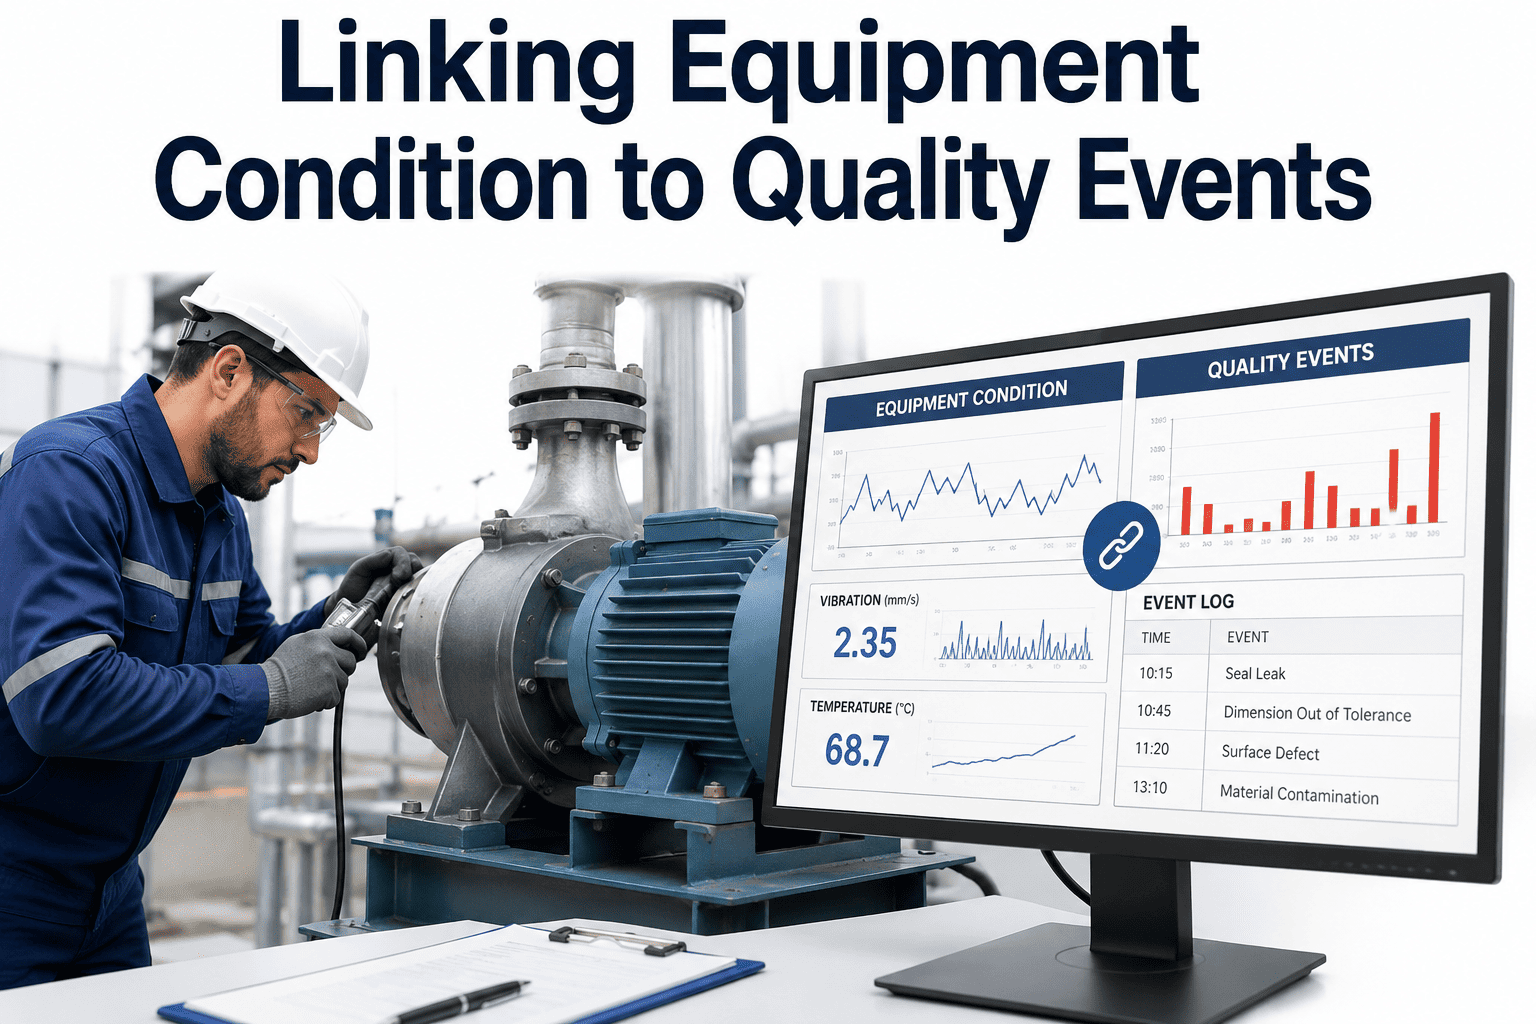
- Link reject data to equipment, shift, and lot
- Root cause analysis via CMMS quality records
- SPC trending to catch drift early
How CMMS Data Drives OEE Improvement in Food Plants
Computerized Maintenance Management Systems have evolved far beyond work order management. Modern CMMS platforms purpose-built for food manufacturing serve as the operational data backbone for OEE tracking, loss analysis, and continuous improvement — connecting maintenance history, equipment sensor data, production records, and quality events into a unified analytical environment.
The operational value of CMMS for OEE optimization lies in its ability to connect data that has historically lived in separate systems — or in no system at all. When a packaging line failure triggers a downtime event, the CMMS links that event to the specific failure mode, the maintenance history of the affected component, the last completed preventive maintenance task, and the production schedule impact. When that analysis is replicated across dozens of downtime events, the highest-impact maintenance investments become statistically clear rather than opinion-based. Sign up free to see how OxMaint's OEE dashboard gives you this visibility across every line in your facility.
Building Your OEE Improvement Roadmap: A Practical Framework
Establish OEE Baseline
Validate data captures all loss types — including minor stops under 5 min. Run automated capture for 3–4 weeks before setting any targets.
Identify Dominant Loss Category
Break OEE into Availability, Performance, and Quality per line. 2–3 loss types usually drive the majority of the gap — focus there first.
Prioritize Bottleneck Assets
OEE loss on a bottleneck constrains the whole line. Use value stream analysis to target assets whose losses directly limit output.
Deploy Targeted Countermeasures
Match the fix to the loss — predictive maintenance for failures, SMED for changeover, kaizen for minor stops. Track all actions in CMMS.
Review Weekly, Adjust Quarterly
Hold weekly OEE reviews with production, maintenance, and quality teams. Refresh improvement priorities every quarter based on trend data.
OEE and Food Safety: Why the Two Programs Must Be Integrated
In food manufacturing, OEE optimization and food safety compliance are often managed as separate programs by separate teams — operations chasing efficiency metrics while quality and food safety manages HACCP compliance and audit documentation. This organizational separation creates a significant blind spot: the decisions made in pursuit of OEE improvement can directly affect food safety outcomes, and food safety requirements (sanitation, allergen changeover, CCP monitoring) are among the largest drivers of OEE loss.
Integrating OEE and food safety management within a single CMMS platform eliminates this blind spot. Changeover time that includes mandatory allergen sanitation verification cannot be compressed below the time required for safe cleaning — but it can be optimized through better pre-staging of cleaning equipment, parallel external changeover tasks, and faster sanitation verification methods. CCP monitoring data that triggers corrective action workflows also generates quality loss events in the OEE quality component — linking food safety deviations to OEE impact and ensuring that corrective actions address both the compliance requirement and the underlying process instability. Book a demo to see how OxMaint unifies OEE tracking and food safety compliance in a single operational platform.
Ready to Close the Gap Between Current and World-Class OEE?
OxMaint gives food manufacturing operations managers real-time OEE visibility, automated loss analysis, and CMMS-driven improvement workflows — across every production line, every shift, every product.
Frequently Asked Questions: OEE in Food Production
What is a good OEE score for food manufacturing?
World-class OEE in food manufacturing is 85% or above, but most facilities average between 55% and 65%. High-speed packaging and meat processing lines typically sit at the lower end, while thermal processing lines score higher. The most useful benchmark is your own trend — consistent improvement matters more than hitting a generic industry number.
How is OEE calculated for a food production line?
OEE = Availability × Performance × Quality. For example: 87.5% availability × 85% performance × 96% quality = 71.4% OEE. Each factor is calculated from actual run time, output rate vs. rated speed, and first-pass good product respectively. Automated CMMS calculation eliminates the errors common in manual spreadsheet tracking.
What causes low OEE in food plants?
The most common causes are extended changeover duration, unrecorded minor stops on packaging lines, and startup rejects after each product transition. Food-specific requirements — allergen sanitation, HACCP monitoring, and mandatory cleaning — add OEE loss complexity not found in other industries. CMMS-based tracking across all six loss categories pinpoints the exact drivers.
Can a CMMS track OEE for food manufacturing lines?
Yes. Modern CMMS platforms integrate with IoT sensors and production equipment to capture availability, performance, and quality data automatically — calculating OEE in real time by line, shift, and product. Loss events are linked directly to maintenance work orders, enabling root cause analysis that connects equipment failures to their production impact.
How does changeover frequency affect OEE in food production?
Each changeover generates simultaneous loss across all three OEE components — downtime (availability), startup rejects (quality), and slow ramp-up (performance). High-SKU operations and contract food manufacturers are most exposed to this compounding effect. Run sequencing to reduce allergen changeover frequency and SMED methodology are the highest-impact countermeasures.
What is the relationship between OEE and food waste reduction?
Every OEE quality loss event — a checkweigher reject, a metal detection failure, a fill weight deviation — is also a food waste event. Improving OEE quality therefore directly reduces waste, supporting both cost reduction and sustainability targets. CMMS root cause data on quality losses makes it possible to eliminate the process conditions generating that waste.