Blister packaging lines are the final gatekeeper before product reaches patients — and when they stop, they stop everything. An FDA Warning Letter citing seal integrity failures or vision inspection downtime can trigger a $2–15 million facility remediation. Yet maintenance teams still manage forming temperatures, sealing parameters, and camera calibration across multiple stations with spreadsheets and paper logs. This article covers every critical maintenance zone on a pharma blister line: forming, sealing, coding, vision inspection, and batch packaging equipment — with PM tasks, failure modes, and the documentation approach that keeps auditors satisfied. If you want structured PM workflows on your blister line before your next batch, start a free trial or book a 30-minute demo with OxMaint's pharma packaging specialist.
Article · Blister Packaging · Pharma Maintenance
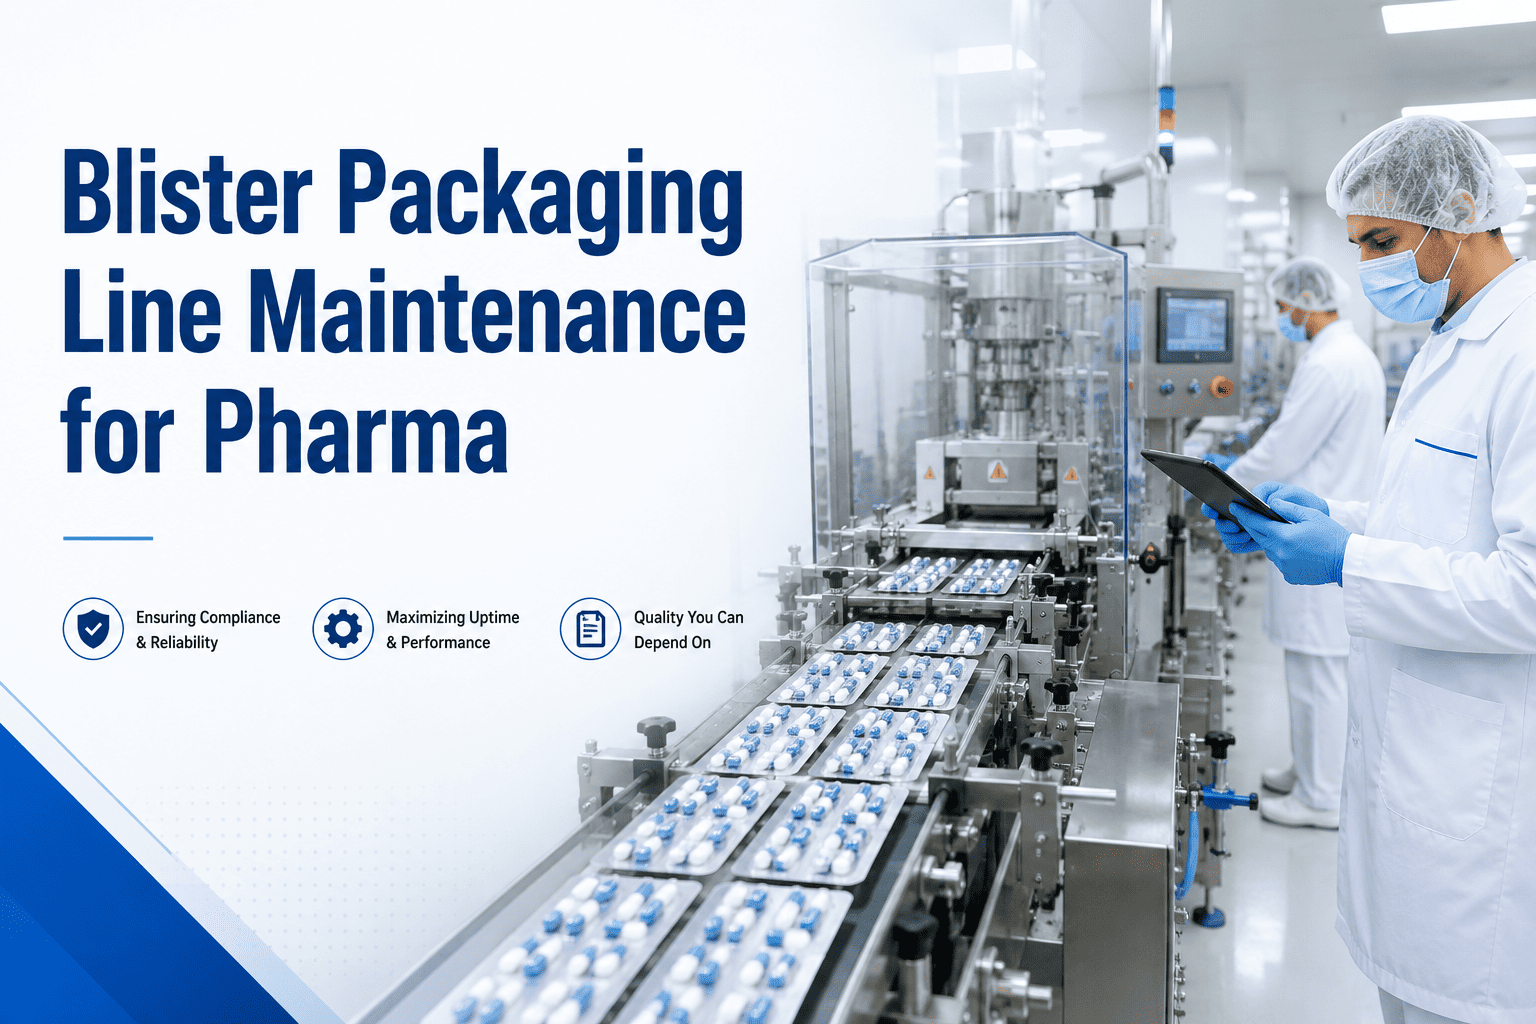
Blister Packaging Line Maintenance for Pharma
Prevent line stoppages with targeted PMs for every station — forming, sealing, coding, vision inspection, and batch packaging — all connected in one audit-ready system.
Regulatory Exposure if Maintenance Fails
$2M – $15M
Average FDA Warning Letter remediation cost per facility action on a pharma packaging line
How a Blister Line Fails: The 5-Station Breakdown
Each station on a blister packaging line has a distinct failure mode. Maintenance that treats the whole line as one system misses station-specific root causes that cause rejected packs, false rejects, and unplanned stops.
01
Forming Station
Top Failure: Uneven cavity depth from temperature drift or worn forming tooling
PM Focus: Forming plate temperature calibration, film tension control, mold surface inspection
02
Sealing Station
Top Failure: Incomplete seal from pressure drop or heat band degradation
PM Focus: Sealing temperature verification, pressure transducer calibration, heat band replacement schedule
03
Coding & Embossing
Top Failure: Misaligned or illegible batch/expiry codes failing vision verification
PM Focus: Print head cleaning, inkjet nozzle verification, laser optics inspection, registration alignment check
04
Vision Inspection System
Top Failure: Camera calibration drift causing false rejects or missed defects
PM Focus: Camera lens cleaning, reference standard verification, defect detection sensitivity confirmation per product
05
Die-Cut & Discharge
Top Failure: Blister card edge cracking from worn cutting blades causing reject rate spike
PM Focus: Blade edge inspection, cutting force measurement, discharge belt alignment, jam detection sensor verification
PM Frequency Matrix
Effective blister line PM is not a single schedule — it is a matrix of station-specific tasks mapped to the correct interval. Here is the complete reference your maintenance team needs.
| Station |
Daily |
Weekly |
Monthly |
| Forming |
Verify forming temperature at startup; check film roll tension |
Inspect forming plate surface; measure cavity depth on 10 sample blisters |
Full mold inspection and dimensional check; thermocouple calibration |
| Sealing |
Record sealing temperature and pressure at batch start and end |
Inspect heat band for delamination or hot spots; check seal jaw alignment |
Replace heat bands per OEM interval; recalibrate pressure transducers |
| Coding |
Run test print and verify batch/expiry readability before batch start |
Clean inkjet print heads or laser optics; verify registration alignment |
Full coding system calibration; replace consumable parts per usage |
| Vision System |
Run reference standard through system; confirm accept/reject accuracy |
Clean camera lenses; verify defect detection sensitivity settings |
Full camera calibration; validate detection against qualification standard blisters |
| Die-Cut / Discharge |
Inspect cut edge quality on 20 sample cards; check discharge belt tracking |
Measure blade edge condition; verify cutting force setting |
Replace worn cutting blades; inspect all transport belts for wear |
Run This Matrix as Automated Work Orders
OxMaint converts station-specific PM schedules into auto-triggered mobile work orders. When a weekly sealing inspection is due, the right technician gets the right task — with prompts, photos, and sign-off — before the batch starts.
Seal Integrity: The Highest-Risk PM Task
Seal failure is the most cited defect in blister line FDA observations. A hermetic seal depends on three validated parameters — all three must be checked at every batch start and logged with the batch record.
Temperature
Validated range: ±3°C of target
If out of range: Stop batch, investigate heat band condition, recalibrate thermocouple before restart
Pressure
Validated range: ±0.5 bar of target
If out of range: Check pneumatic circuit for leaks, verify pressure transducer calibration status
Dwell Time
Validated range: per product SOP (typically 0.3–1.2 sec)
If out of range: Verify PLC recipe matches batch SOP, inspect cam drive timing
Seal integrity testing method (dye ingress, vacuum decay, or bubble emission) must be performed on samples from each production batch and results logged in the batch record with operator sign-off.
Vision Inspection: Maintenance That Protects Quality
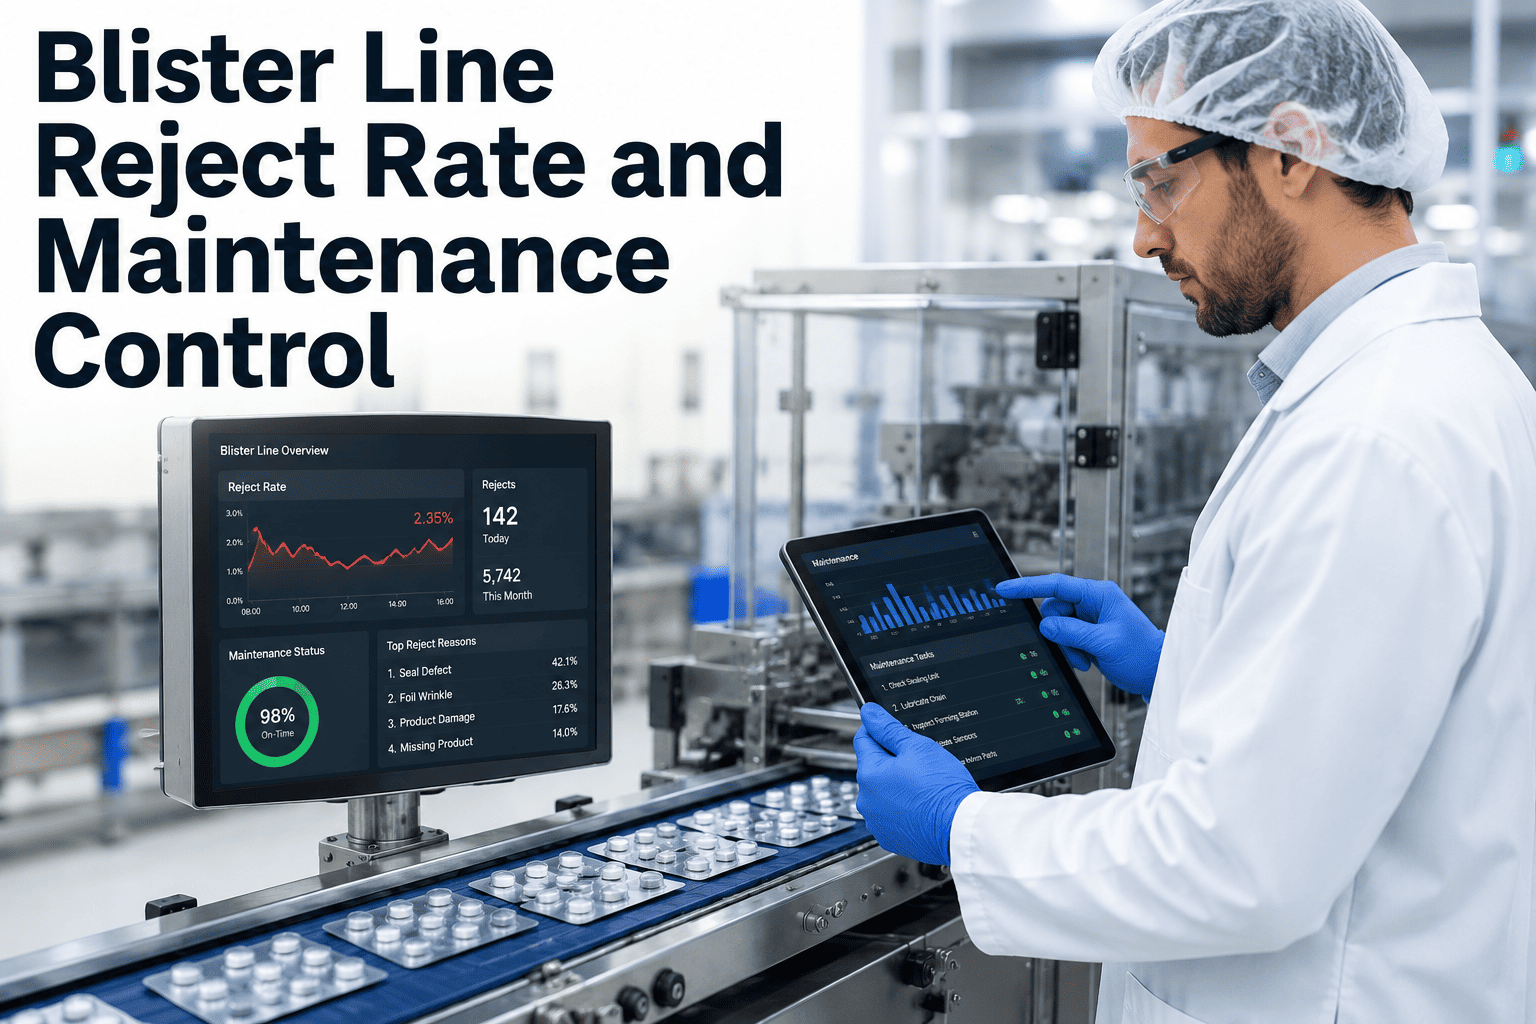
Vision inspection systems catch missing tablets, foil defects, and coding errors — but only when they are properly maintained. A camera that drifts out of calibration becomes a liability, not a safeguard.
Daily
Reference Standard Verification
Pass known-defective reference blisters through the system before each batch. System must correctly reject missing-tablet, foil-defect, and code-error samples. Document pass/fail in batch record.
Weekly
Lens Cleaning & Sensitivity Check
Clean camera lenses with compressed air and lint-free wipes. Verify detection sensitivity has not drifted — compare false reject rate and missed defect rate against qualification baseline.
Monthly
Full Camera Calibration
Calibrate all cameras against validated reference images for each product on the line. Calibration records must include date, technician, result, and next-due date — stored in CMMS, not in local machine memory.
Expert Review
MK
Michael Krause
Packaging Systems Engineer · 16 Years · Solid Oral Dosage & Blister Line Integration, Europe & US
"The fastest way to lose a batch on a blister line is to let sealing temperature drift unchecked for two hours during a long production run. Temperature creep from a degrading heat band is slow enough to miss manually but fast enough to compromise every pack produced in that window. The second fastest way is vision inspection calibration drift — your system starts accepting defective packs because no one ran the reference standard that morning. Both failures are 100% preventable with a digital PM system that auto-escalates overdue tasks. Every plant I have worked with that switched from paper logs to CMMS-driven PM saw rejected pack rates drop within 60 days."
★★★★★
Frequently Asked Questions
What are the most common causes of blister line stoppages in pharma manufacturing?
The three most common causes of unplanned blister line stops are seal integrity failures (heat band wear or temperature drift), vision inspection false-reject spikes (camera calibration drift or dirty lenses), and coding system failures (inkjet nozzle clogging or laser optic contamination). All three are preventable with the correct PM schedule — temperature and pressure records at every batch start, daily reference standard verification for vision systems, and weekly print head cleaning for coding units. When maintenance tasks are tracked in a CMMS with automatic overdue escalation, these stops are caught before the batch, not during it.
Start a free trial to set up your first blister line PM schedule.
How often does a blister line vision inspection system need to be calibrated?
Vision inspection systems on pharma blister lines require a daily reference standard verification (passing known-defect blisters through the system to confirm correct detection), a weekly lens cleaning and sensitivity check comparing false reject rate against the qualification baseline, and a full product-by-product camera calibration at least monthly. If the line runs multiple products, each product recipe must be separately validated and calibration records must be stored in a system that is accessible for audits — not on a local machine hard drive. Under FDA 21 CFR Part 11, these records must be time-stamped, attributable, and retrievable.
Book a demo to see how OxMaint manages vision system calibration records.
What GMP documentation is required for blister packaging line maintenance?
GMP documentation requirements for a blister packaging line include: a batch record entry confirming PM status and line readiness before each production batch; seal integrity test results (temperature, pressure, dwell time) at batch start and end; vision inspection reference standard verification results logged per batch; coding system print verification before each batch; and a formal PM work order for every scheduled maintenance task with date, technician, findings, and corrective actions. Each document must be signed, dated, and retained for the product shelf life plus one year under 21 CFR Part 211. Digital CMMS records that auto-generate from completed mobile work orders satisfy these requirements without manual data entry or paper handling.
Can OxMaint manage PM schedules for all stations on a multi-station blister packaging line?
Yes. OxMaint supports asset hierarchies where each station on a blister line — forming, sealing, coding, vision inspection, and die-cut — is a separate asset with its own PM schedule, calibration record, and work order history. When a daily sealing temperature check is due, the system creates a mobile work order for the on-shift technician with specific prompts, parameter entry fields, and photo capture. Weekly and monthly tasks auto-generate on schedule without a planner having to manually create them. All completed work orders are linked to the asset record and are immediately available for audit review.
Start a free trial and have your blister line PM schedule configured within the first day.
Prevent Your Next Blister Line Stoppage — Starting This Week
OxMaint gives pharma maintenance teams station-level PM schedules, mobile task completion, seal integrity logging, and vision system calibration records — all in one audit-ready platform that deploys in days.