A rotary kiln failure does not announce itself — it builds silently through weeks of subtle indicators that unmaintained plants miss entirely. When the kiln finally stops, the average cost is $180,000–$400,000 per day of lost production, emergency repair mobilization, and refractory damage that compounds with every hour of uncontrolled cool-down. With a global installed base of over 2,000 active cement kilns and median refractory campaigns lasting just 9–14 months, the question is never whether your kiln will require intervention — it is whether your maintenance team will be ready before or after the failure. This guide gives you the complete failure prevention framework: component-by-component maintenance protocols, early warning indicators, inspection intervals, and the CMMS-linked monitoring architecture that separates reactive cement plants from those running 340+ days per year. Start your free Oxmaint trial and get kiln-specific asset templates deployed in under 48 hours.
Kiln Anatomy: The 7 Critical Maintenance Zones
Every rotary kiln failure originates in one of seven distinct zones. Understanding the failure modes specific to each zone — and the monitoring strategy required to detect them early — is the foundation of effective kiln maintenance. Book a demo with Oxmaint to see how these zones map directly into a structured asset hierarchy in the CMMS.
Feed End & Inlet Seal
Tyre & Riding Ring Assembly
Refractory Lining
Main Drive & Girth Gear
Burning Zone & Burner
Discharge End & Nose Ring
Build Your Complete Kiln Asset Hierarchy in Oxmaint — Pre-Configured Templates Included
Every zone, component, inspection task, and failure mode documented above is pre-loaded in Oxmaint's cement plant templates. Deploy your kiln maintenance program in days, not months — with mobile checklists, automated PM scheduling, and real-time shell scanner integration.
Failure Mode Risk Matrix: Prioritizing Your Kiln Maintenance Effort
Not all kiln failure modes deserve equal maintenance investment. This risk matrix plots 14 common kiln failure modes by consequence severity and detection lead time — the two dimensions that determine how aggressively to monitor and maintain each. Sign up for Oxmaint to configure automated alerts for all high-consequence failure modes listed below.
The Kiln Maintenance Schedule: Weekly to Annual Intervals
Effective kiln maintenance operates on four overlapping time cycles. The daily and weekly cycles are executed by operators and maintenance technicians. Monthly and shutdown cycles require specialist involvement. All four cycles must be documented in the CMMS with timestamped sign-offs to create the audit trail that satisfies ISO 45001, insurance requirements, and internal reliability reviews. Book a demo to see Oxmaint's automated kiln PM scheduling in a live demonstration.
CMMS-Linked Monitoring: The Early Warning Architecture
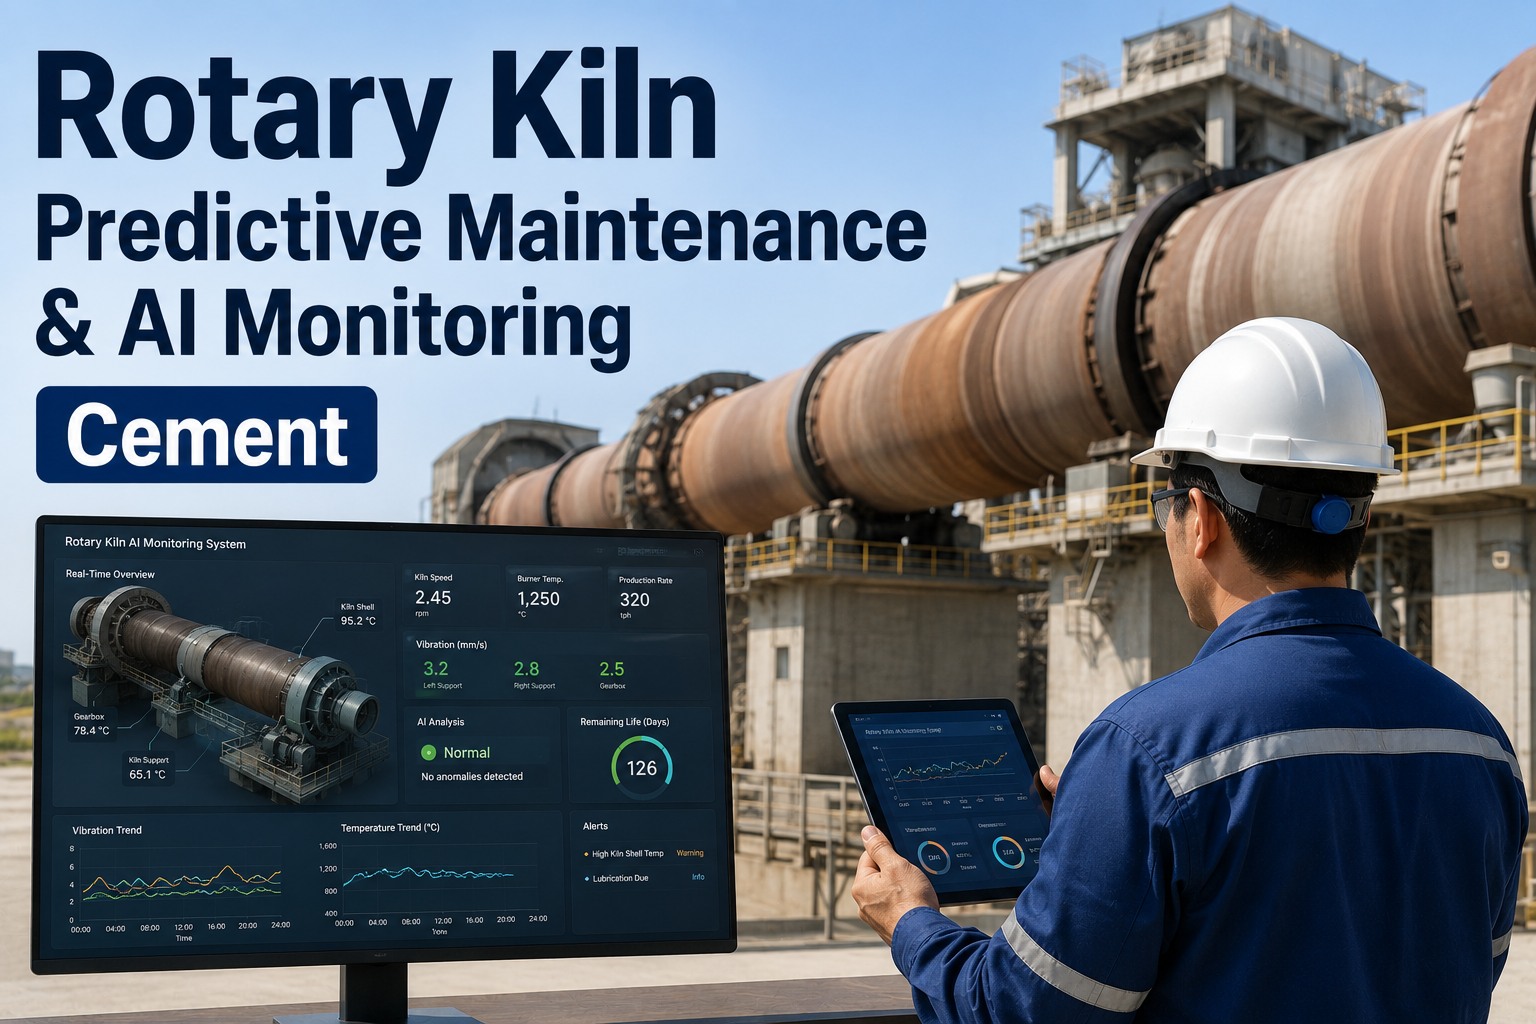
The difference between a planned 5-day refractory repair and an emergency 21-day campaign is almost always the quality of the monitoring system — specifically, whether kiln data flows into a CMMS that creates work orders before conditions become critical. Sign up for Oxmaint to connect your kiln monitoring sensors to an automated work order system today.
Infrared Shell Scanner
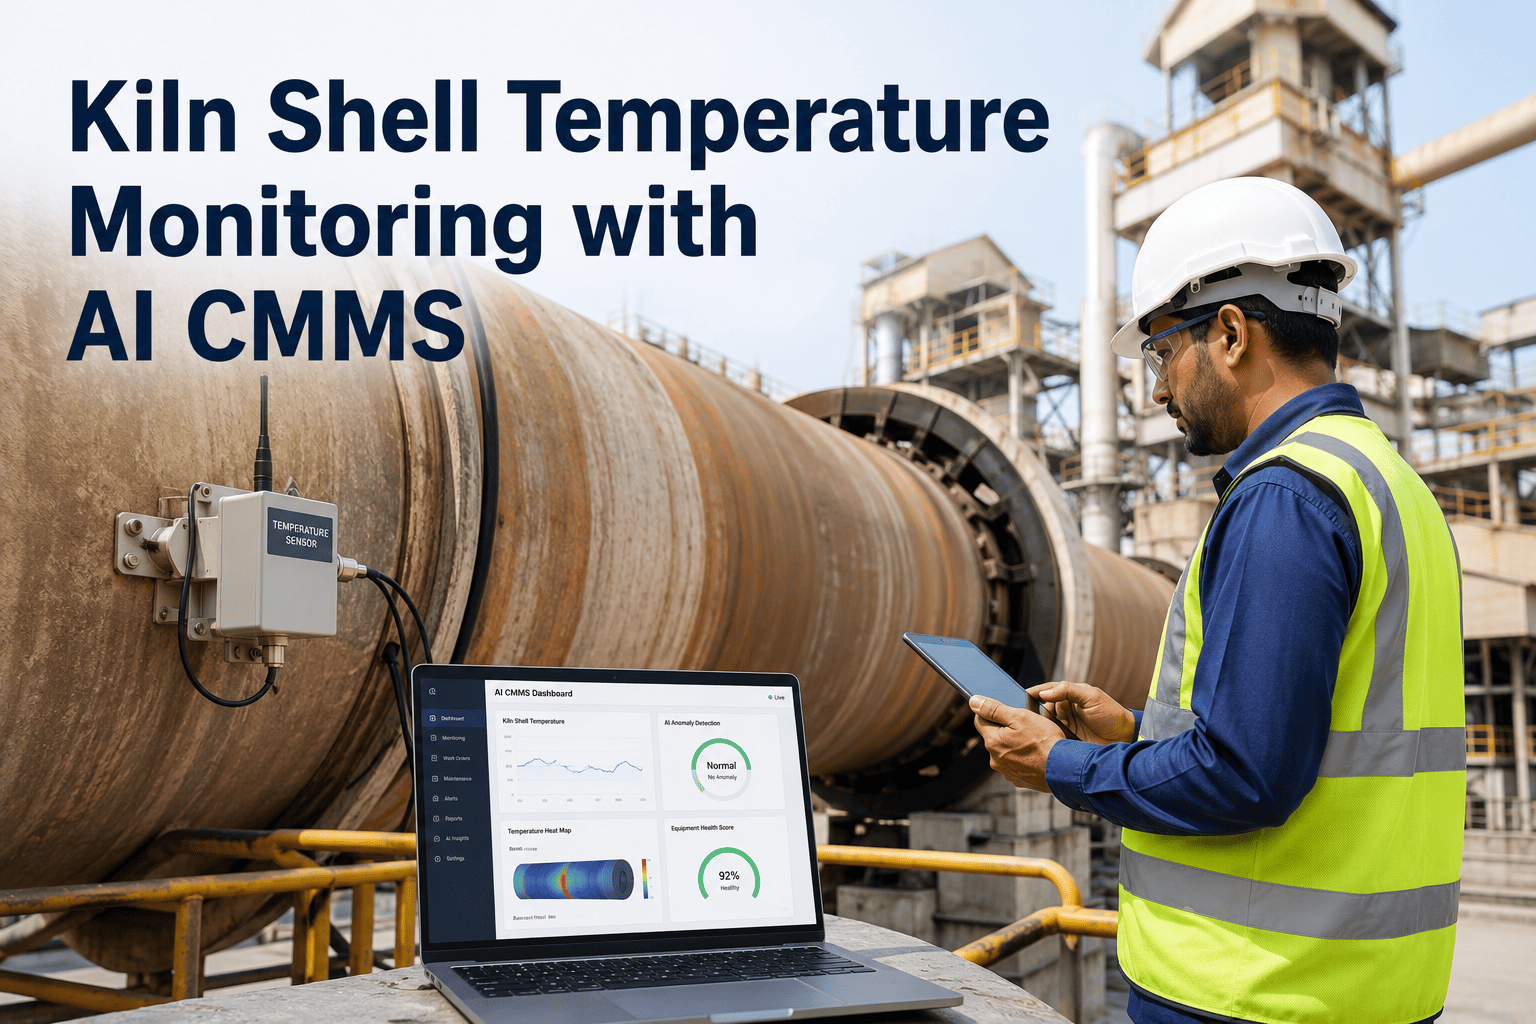
Rotating IR camera provides 360° shell temperature profile every revolution. Detects hot spots from brick thinning weeks before failure. CMMS integration creates graded alerts: Advisory at +30°C above baseline, Warning at +60°C, Emergency stop recommendation at +100°C above zone baseline.
Bearing Vibration Monitoring
Accelerometers on all pinion bearings and support roller bearings measure velocity RMS and high-frequency envelope signals. Trending algorithms detect gear mesh frequency shifts that indicate tooth wear, and sub-synchronous frequency components that indicate bearing cage damage — typically 14–21 days before audible noise appears.
Kiln Drive Power Monitoring
Main drive motor current and calculated torque are the most sensitive indicators of coating ring formation, material buildup, and internal blockage. A 15% torque increase sustained over 2+ hours indicates coating ring growth requiring intervention. Sudden torque spikes often precede large coating ring collapses that damage brickwork.
Tyre Migration Sensor
Linear variable differential transformers (LVDTs) or laser displacement sensors measure tyre axial position continuously. Migration rate trending identifies whether filler bars are properly sized — a migration rate above 2mm/week indicates undersize filler bars that will require attention at next convenient stop before causing refractory damage.
Oxmaint Converts Shell Scanner Alerts, Vibration Spikes, and Drive Torque Anomalies Into Prioritized Work Orders — Automatically
Pre-built OPC-UA connector pulls data from your DCS historian. Configurable alert rules create, assign, and escalate work orders without operator intervention. Every anomaly documented, every response tracked. Prove it in a 30-minute live demo.
Frequently Asked Questions
How long should a cement kiln refractory campaign last, and what determines campaign life?
Refractory campaign life for a modern dry-process cement kiln ranges from 9 to 18 months, with world-class operations regularly achieving 14–18 month campaigns. The primary determinants of campaign life are: (1) Burning zone coating stability — stable coating insulates brick from peak temperatures and is the single biggest factor; (2) Alkali and sulfur loadings in the raw materials and fuels — high-alkali inputs chemically attack brick structure; (3) Kiln shell straightness and ovality — a kinked or oval shell mechanically stresses bricks cyclically with every revolution; (4) Thermal cycling frequency — every emergency stop and relight costs 2–4 weeks of campaign life; (5) Brick quality and installation — incorrect brick geometry, improper mortar thickness, or ring installation errors create stress concentration points. Plants achieving 18+ month campaigns combine stable raw materials, excellent shell alignment, AI-controlled burning zone temperatures within ±20°C, and CMMS-managed brick replacement planning that replaces targeted zones at planned stops before failure.
What is tyre slip and what is the correct measurement method?
Tyre slip is the relative rotational movement between the kiln tyre (riding ring) and the kiln shell. Because the tyre sits loosely on filler bars rather than being rigidly fixed to the shell, a small amount of slip is necessary to allow differential thermal expansion — typically 0.5–1.5% of peripheral velocity. Measurement is performed by painting a chalk mark on both the tyre inner surface and the shell plate simultaneously, then measuring the gap after one full revolution (usually 24 hours of operation). The correct measurement formula is: Slip (%) = (Gap distance / Shell circumference) × 100. Slip below 0.3% indicates overtight filler bars causing mechanical stress. Slip above 2% indicates undertight filler bars, causing excessive migration and shell bending moment. Both conditions require filler bar adjustment at the next planned stop. Weekly measurement and trending in the CMMS allows early detection of changing conditions before they become structural problems.
How should we respond to a kiln shell hot spot detected by infrared scanning?
Kiln shell hot spot response should follow a graded protocol based on temperature deviation from the zone baseline. For a temperature 30–60°C above baseline (Advisory level): increase shell scanner scan frequency to continuous review, enhance coating by temporarily increasing feed rate or adjusting burning zone conditions, and schedule inspection at next planned stop — do not yet interrupt production. For 60–100°C above baseline (Warning level): alert plant management, begin preparations for emergency stop, adjust kiln operating conditions to reduce thermal load on the affected zone, and plan for stop within 24–48 hours if temperature continues rising. For greater than 100°C above baseline (Emergency level): initiate controlled kiln stop immediately — continuing to run risks shell deformation, tyre damage, and catastrophic refractory collapse that converts a $200K repair into a $2M+ campaign. The cost of an unplanned 2-day stop is always less than the cost of a failed 21-day emergency repair.
What causes girth gear tooth failure and how can it be prevented?
Girth gear tooth failures in cement kilns occur through four mechanisms: (1) Pitting fatigue — subsurface crack initiation from contact stress exceeding the material endurance limit, typically from gear misalignment or overloading; (2) Micropitting — abrasive wear from inadequate film thickness in the lubricant, often caused by incorrect viscosity selection or contaminated lubricant; (3) Spalling — adhesive wear when the lubrication film breaks down under high tooth loads; (4) Tooth bending fatigue — cyclic bending stress from kiln shell ovality creating variable load, or from shock loads during coating ring collapses. Prevention requires: (a) Annual gear alignment verification and correction, (b) Lubricant viscosity matched to operating temperature and pitch line velocity, (c) Continuous drive motor current monitoring to detect load spikes from coating ring events, (d) Kiln shell ovality correction to eliminate cyclic load variation, and (e) Monthly tooth surface inspection with dye penetrant on any pitted areas. Vibration envelope analysis on the pinion bearings provides 14–21 days of warning of gear mesh deterioration — time to source parts and plan a controlled stop.
How do we plan a kiln shutdown to maximize campaign life at minimum cost?
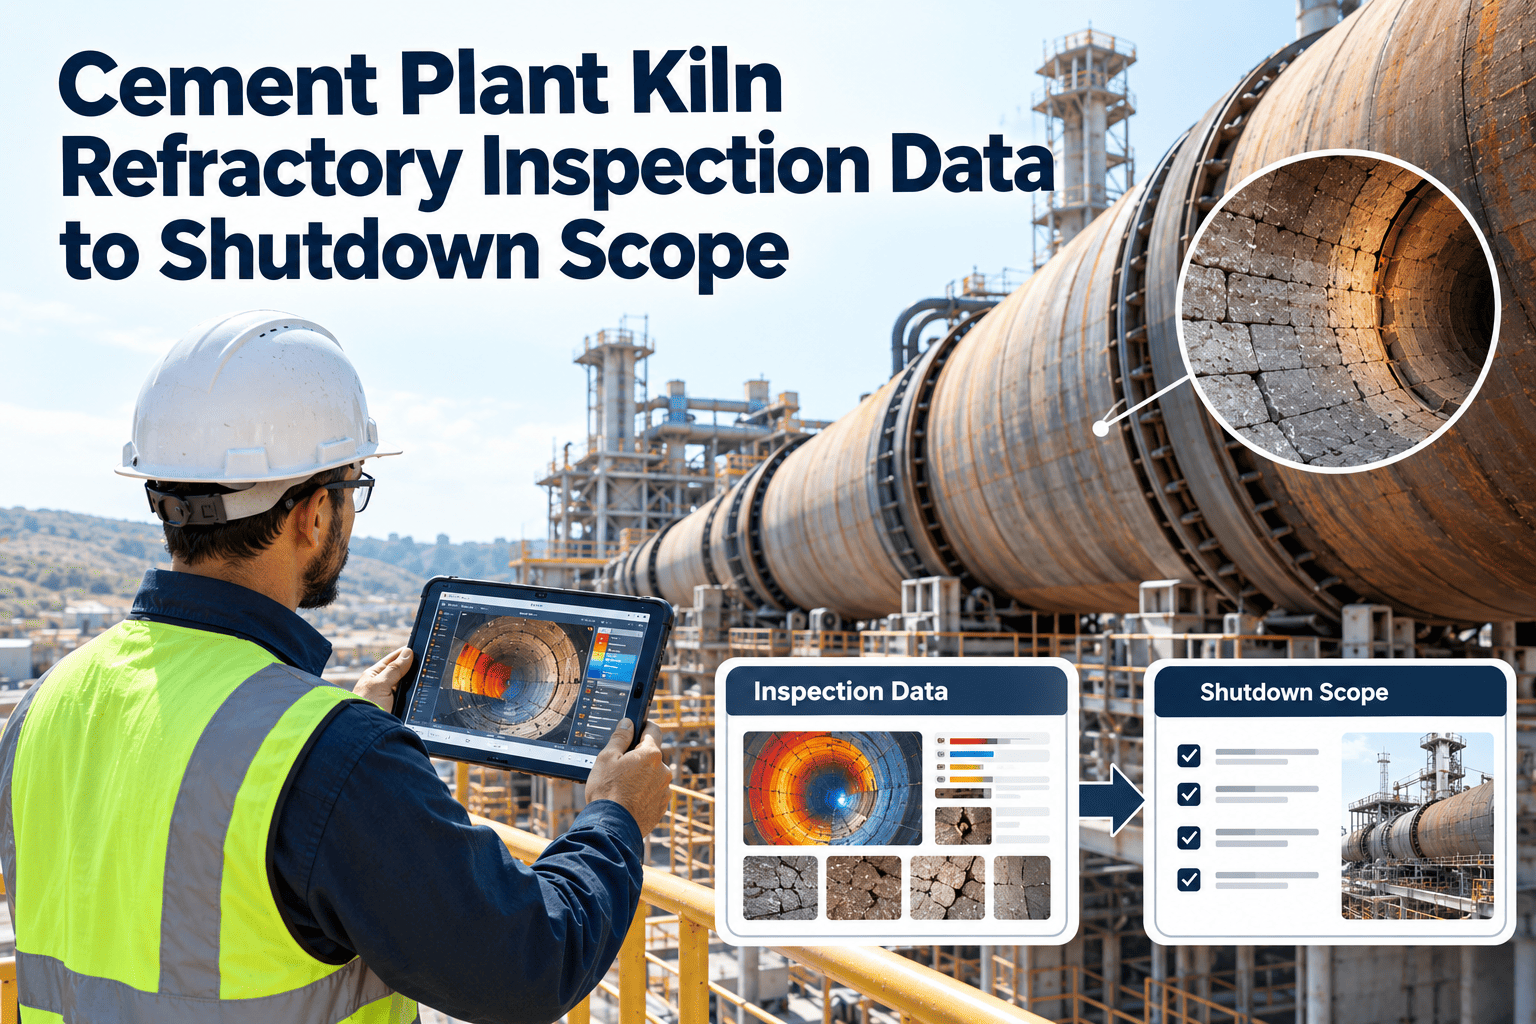
Optimal kiln shutdown planning uses the CMMS accumulated maintenance data to define a scope that addresses all items at their natural end-of-life simultaneously — eliminating the cost of multiple short stops. The process starts 12 weeks before planned stop date: (1) Extract remaining brick life estimates by zone from shell scan trend data; (2) Review monthly bearing condition assessments to identify any components near end-of-life; (3) Compile outstanding work orders deferred from running repairs; (4) Survey mechanical wear items (rollers, seals, filler bars) against replacement criteria. This analysis defines the shutdown scope. Material procurement should be finalized 8 weeks before stop. Contractor mobilization should be planned 4 weeks before. The CMMS shutdown work order package — with sequenced tasks, resource assignments, and materials linked to each work order — should be issued 2 weeks before. Plants using this CMMS-managed shutdown planning approach consistently extend campaign life by 15–25% compared to reactive shutdown scoping.
What is the correct kiln alignment procedure and how often should it be performed?
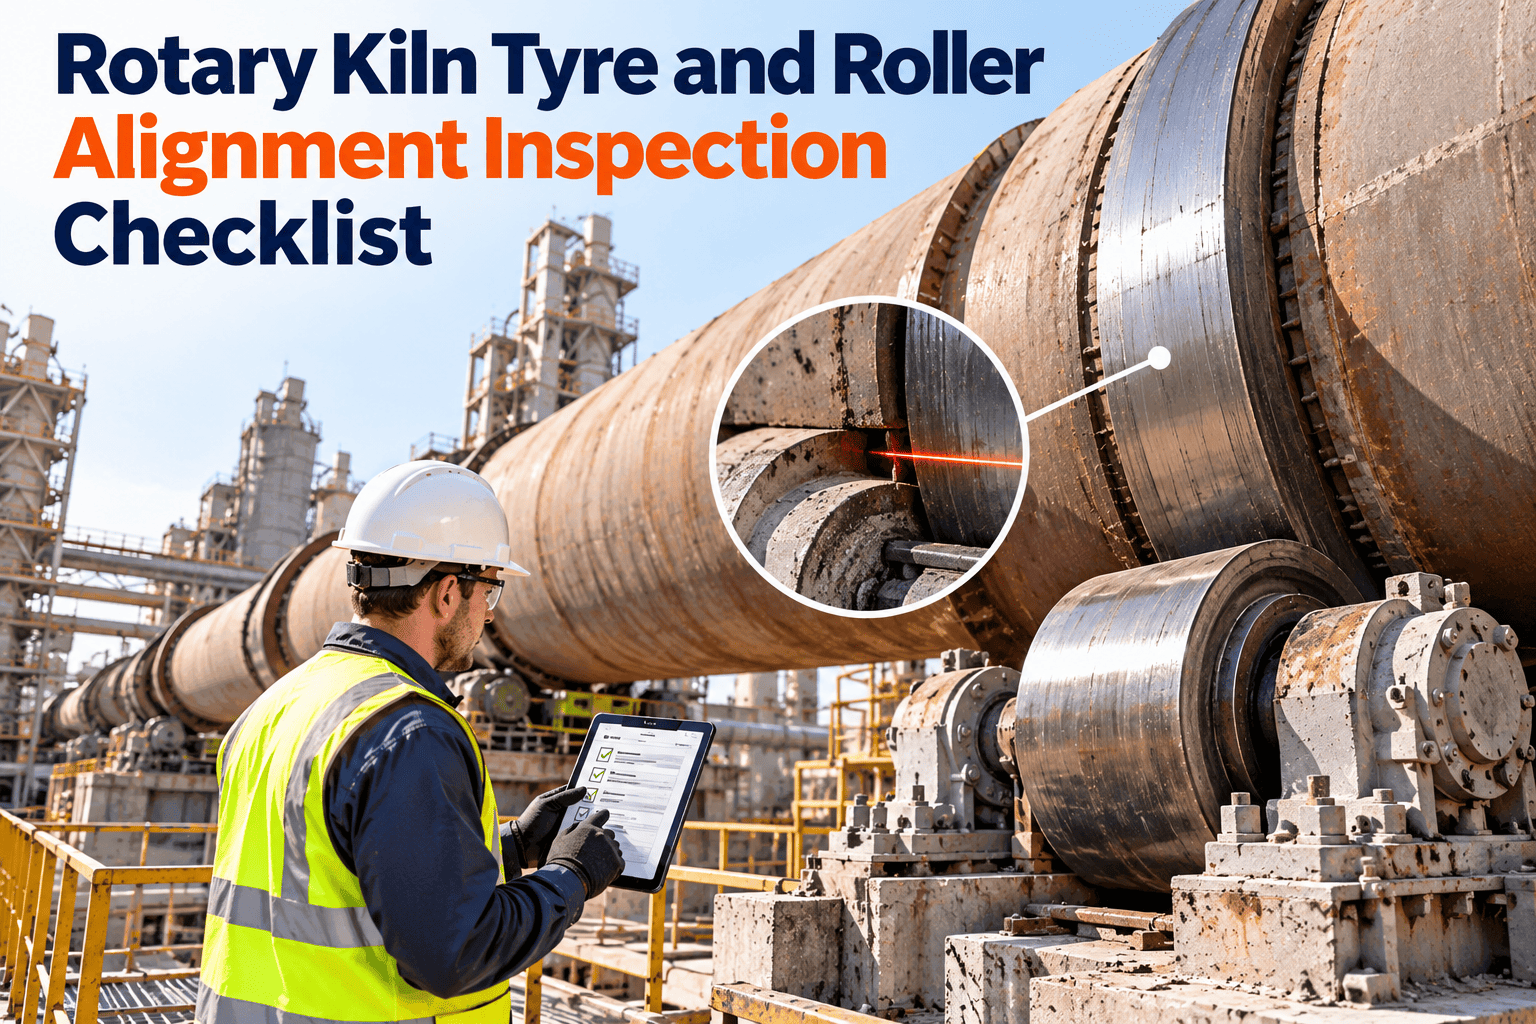
Kiln alignment is the process of ensuring all three (or four) support stations have their tyre contact points on a single theoretical axis — the kiln centerline. Misalignment causes uneven load distribution between support rollers, accelerates tyre and roller wear, creates shell bending moments that crack refractory, and can cause thrust roller overloading leading to axial displacement. The recommended procedure uses a laser tracker or optical alignment instrument to measure the geometric center of each tyre at four circumferential positions during slow rotation. Results are plotted as a "crank" (lateral offset) and "sag" (vertical deflection) diagram. Acceptable tolerances are typically ±2mm lateral and ±3mm vertical deviation from the theoretical straight line. Corrective adjustment is made by hydraulically adjusting support roller skew angles — a small skew moves the tyre axially, correcting lateral position. Alignment should be performed: at every major shutdown, after any emergency stop involving refractory repair, whenever thrust roller load imbalance exceeds 15% between stations, and whenever tyre migration rate changes significantly. Full alignment surveys require 4–8 hours of kiln down time and should always be included in shutdown scope planning in the CMMS.
How does a CMMS specifically improve kiln reliability and extend campaign life?
A CMMS improves kiln reliability through five mechanisms that manual systems cannot replicate. First, it eliminates missed inspections — automated PM scheduling ensures every daily, weekly, and monthly task is assigned, executed, and documented regardless of shift changes or personnel turnover. Second, it enables trend detection — when daily tyre migration readings are entered consistently, the CMMS can flag a rate change within 3–5 days, long before it becomes visible to any individual technician reviewing single data points. Third, it creates institutional memory — failure history, repair records, and component replacement dates are preserved even when experienced technicians retire or transfer. Fourth, it integrates sensor data — when shell scanner alerts, vibration spikes, and torque anomalies automatically create work orders, response time shrinks from hours to minutes. Fifth, it optimizes shutdown scope — accumulated condition data from the entire running campaign produces a data-driven shutdown scope that replaces components at their natural end-of-life rather than on arbitrary time intervals, reducing both under-maintenance and over-maintenance costs simultaneously.
Every Inspection, Every Alert, Every Shutdown — Managed in One Platform Built for Cement Plants
Oxmaint's kiln maintenance module includes pre-built zone hierarchies, inspection checklists for all 7 critical zones, automated PM scheduling across daily to shutdown cycles, shell scanner alert integration, and ISO 45001-compliant audit trails. Deployed in cement plants across 3 continents.