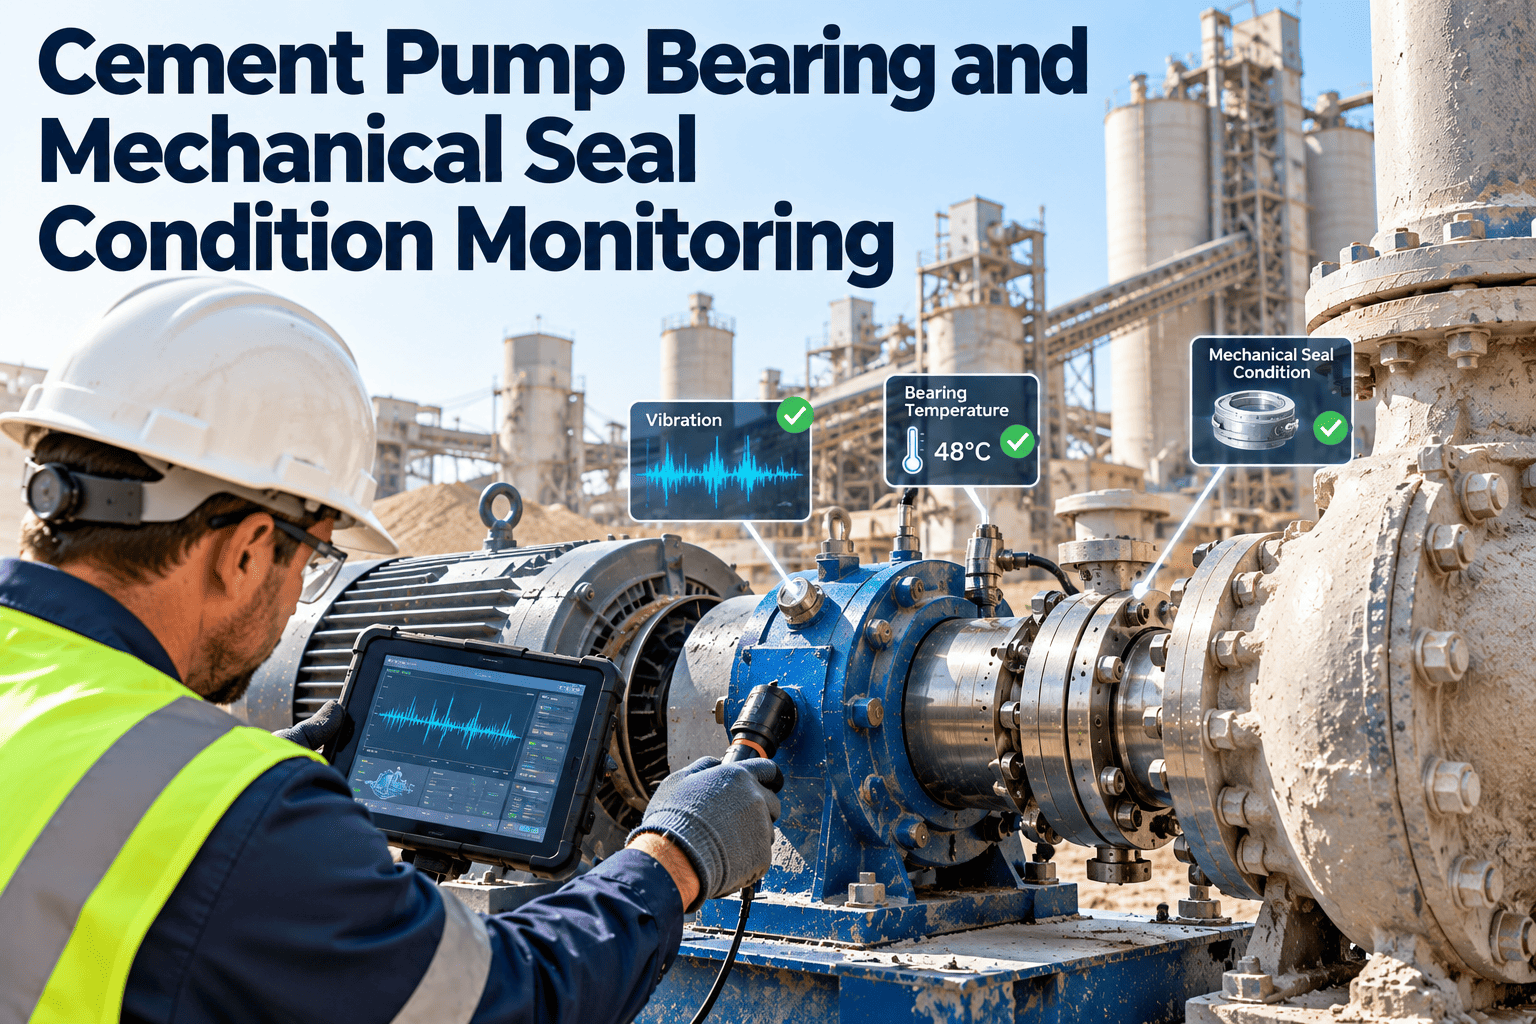
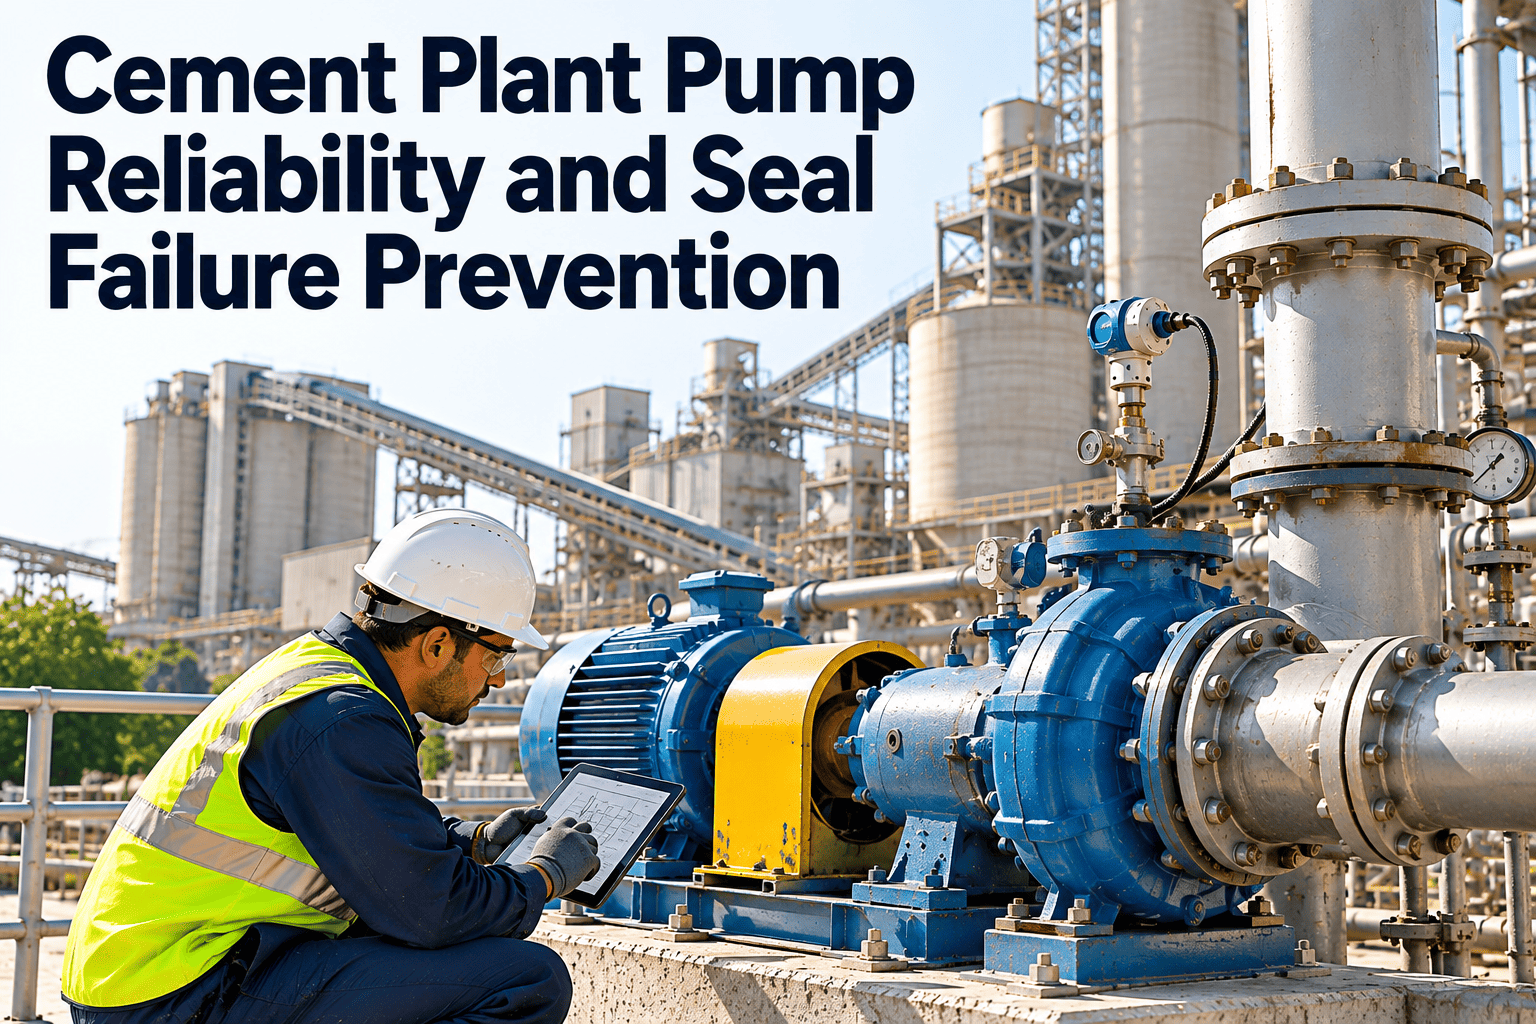
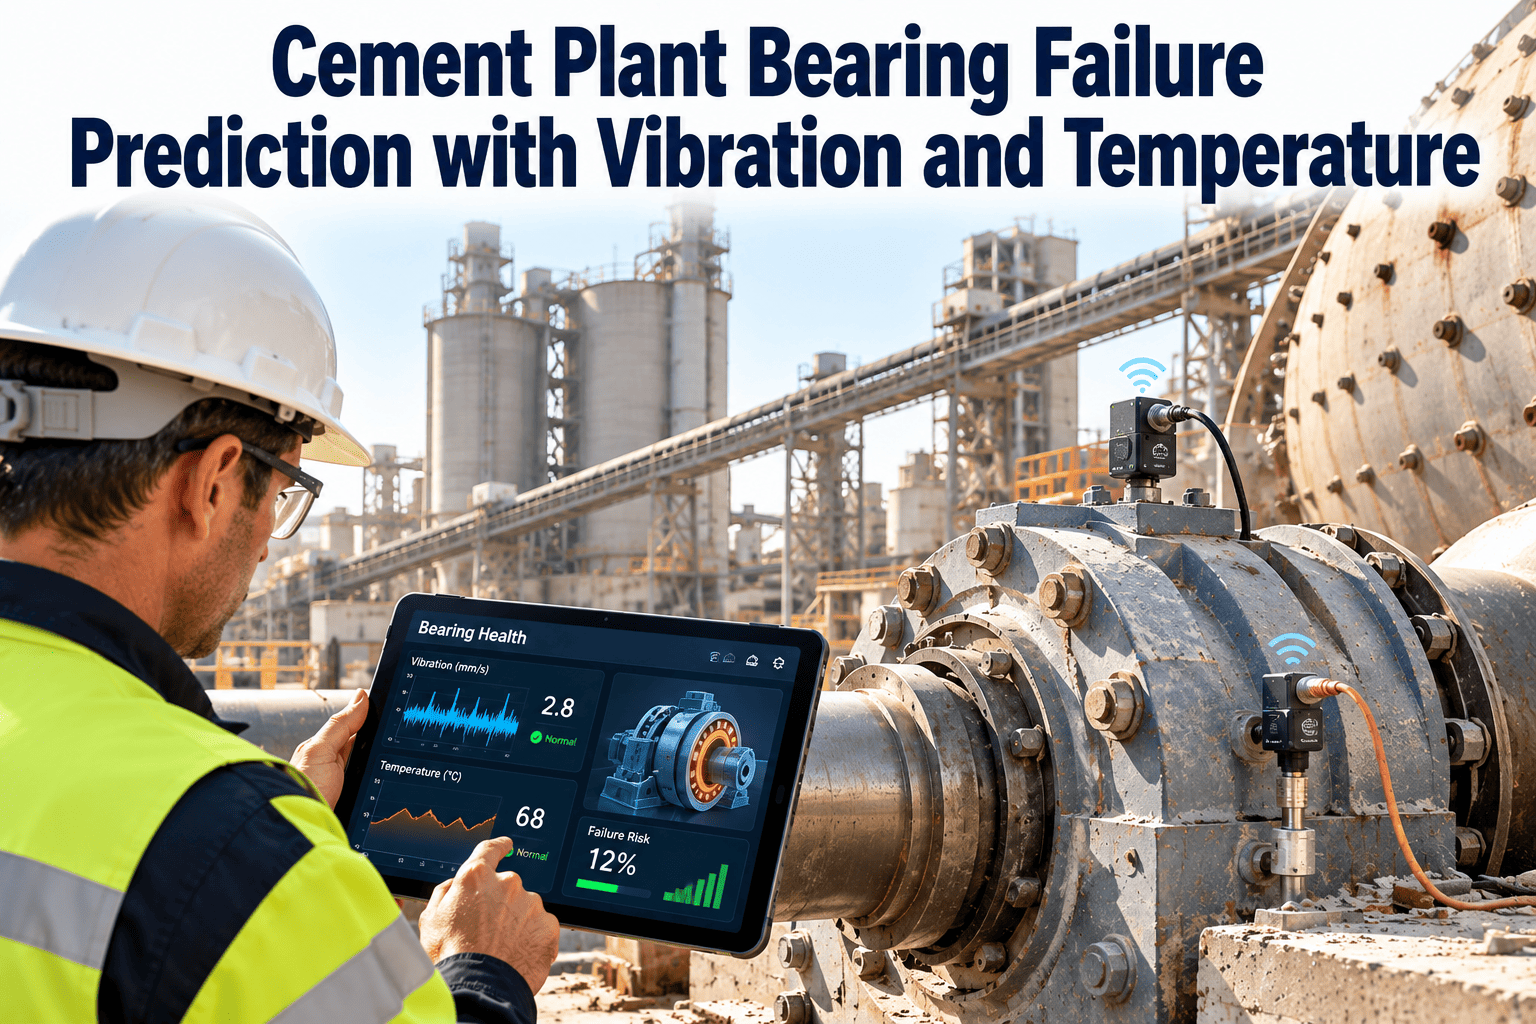
Pumps rarely get the attention that kilns and mills do, yet a failed cooling water pump or a leaking slurry pump seal can force a cement line to reduce load or stop. Bearings and mechanical seals are the two most common weak points, and both give warning long before they fail. Vibration, temperature, leakage and lubricant condition tell a clear story when they are trended together. This guide covers practical bearing and seal monitoring for cement plant pumps, and how a CMMS platform turns those readings into planned work.
Utilities and Pumps
Cement Pump Bearing and Mechanical Seal Condition Monitoring
Detect bearing wear, seal leakage and lubrication problems early, and schedule repairs before a pump takes a process line with it.
DriverMotor current, winding and bearing temperature
CouplingAlignment, guard condition, vibration at running speed
Bearing housingVibration, temperature, oil level and condition
Mechanical sealLeakage, flush flow, face temperature
Casing and impellerPressure, flow, cavitation noise, wear
Where pumps matter in a cement plant
Pump duties differ across the plant, and so does the consequence of failure. Knowing the duty helps you choose the right monitoring effort.
Cooling water systemsServe gearboxes, bearings, compressors and kiln equipment. A loss can force load reduction.
Gas conditioning and spraySupply water to conditioning towers, protecting filters and fans from excess temperature.
Fuel and oil handlingMove fuel oil and lubricants where leakage creates fire and environmental risk.
Slurry and sump dutiesHandle abrasive solids in drainage, washdown and quarry dewatering, where wear is fast.
Hydraulic and lubrication unitsSupport kiln drives, roller presses and crushers, where pressure loss risks equipment damage.
How bearings and seals fail
Most bearing and seal failures have causes that are visible earlier than the failure itself. The table links each mechanism to its early signal.
| Component | Failure mechanism | Early signal | Common root cause |
|---|
| Rolling bearing | Surface fatigue and spalling | Rising high-frequency vibration, then temperature | Overload, misalignment, poor lubricant condition |
| Rolling bearing | Lubricant breakdown | Temperature rise, darkened or contaminated oil | Wrong grade, over- or under-lubrication, heat |
| Rolling bearing | Contamination damage | Water or particles in oil, noise changes | Failed bearing isolators, dust, washdown ingress |
| Mechanical seal | Face wear or damage | Increasing leakage, visible weeping at the gland | Abrasive solids, dry running, poor flush |
| Mechanical seal | Overheating of faces | High seal chamber temperature, flush alarms | Blocked flush line, low flow, process heat |
| Mechanical seal | Shaft movement damage | Seal leakage with vibration at running speed | Misalignment, imbalance, shaft deflection |
| Pump as a whole | Cavitation | Gravel-like noise, erratic pressure, broadband vibration | Low suction head, blocked strainer, wrong operating point |
Symptom to likely cause
Operators and technicians often notice symptoms first. A shared decoder helps them record the right observation and choose the right next check.
Warm bearing housingCheckOil level and condition, alignment, load, lubricant type
Dripping at the seal glandCheckSeal face wear, flush supply, shaft condition
Rising vibration at one bearingCheckBearing condition, looseness, coupling alignment
Noise like gravel in the casingCheckSuction conditions, strainer, operating flow
Milky or dark oilCheckWater ingress, overheating, contaminated oil
Repeated seal failuresReviewFlush plan, solids content, installation practice, shaft runout
Turn pump readings into planned repairs
Record bearing and seal findings against each pump, and let history show which assets need attention first.
A monitoring ladder from walk-around to online sensors
Not every pump needs sensors. Match the technique to the criticality, starting with simple routes and adding instruments where failure is costly.
Operator roundsLook, listen and feel. Record leakage, noise, oil level and obvious heat.
Handheld readingsRoute-based vibration, temperature and ultrasound at fixed points, on a fixed interval.
Lubricant analysisOil samples for contamination, wear particles and condition on larger or critical pumps.
Online monitoringPermanent vibration and temperature sensors on critical or hard-to-reach pumps, with alerts.
Seal environment and flush control
A seal is only as good as its environment. Many early seal failures trace to the flush arrangement rather than the seal itself.
What to inspect on the seal systemFlush line flow and temperatureStrainers, orifices and cyclone separators for blockageQuench or barrier fluid level and conditionLeakage at the gland and drain pointsSeal chamber pressure compared with design
What to record every timePump tag and duty at the time of readingLeakage description and amount, using a simple scaleSeal type, installation date and failure historyOperating conditions, including dry run eventsPhotos for any change since the last visit
Turning readings into alarm bands
Alarm limits should reflect the pump, speed and baseline. Use OEM guidance and standards as a starting point, then adjust using site history.
NormalReadings sit near baseline. Continue the routine.
WatchA clear upward trend. Shorten the reading interval and inspect lubrication and alignment.
Plan repairTrend continues or a second indicator agrees. Raise a work order and check parts.
Act nowRapid change, high temperature or heavy leakage. Switch to the standby and isolate.
Pump route inspection checklist
01Confirm the pump is running at the expected pressure and flow
02Record vibration and bearing temperature at the same points each time
03Check oil level, color and sight glass condition
04Inspect the seal for leakage, noise and flush line status
05Look at the coupling, guard and base bolts
06Listen for cavitation, rubbing or changes in sound
07Record anything unusual with a photo and raise a request if needed
The condition-based repair loop
Monitoring only pays when findings lead to timely work. The loop below shows the path from a reading to a recorded repair.
1Reading logged
2Trend flagged
3Work order raised
4Parts reserved
5Repair done
6Cause recorded
Run-to-failure versus condition-based pump care
TopicRun to failureCondition-based
TimingRepair after the pump stopsRepair when trends justify it
SparesUrgent purchase at premium costPlanned stocking by failure history
Collateral damageShaft and housing damage is commonBearings and seals replaced earlier
Process impactUnplanned load loss or stopSwitch to standby on your terms
LearningCause often unrecordedCause and action stored on the asset
KPIs for pump reliability
Seal life by pumpShows which duties need a better seal plan or material.
Bearing replacements by causeSeparates lubrication, contamination and alignment issues.
Planned vs unplanned pump workIndicates how well early findings become scheduled jobs.
Mean time between repairsTracks improvement after process or practice changes.
Route completionConfirms readings are collected on schedule, not only when convenient.
How Oxmaint supports pump condition monitoring
Oxmaint maintenance software helps cement teams keep pump readings, work orders and parts in one record.
Asset recordsStore pump, bearing and seal details with repair history by tag.
Inspection routesBuild mobile checklists for rounds with readings, notes and photos.
Corrective work ordersConvert a failed check into a work order assigned to the right crew.
Preventive schedulesPlan lubrication, alignment checks and seal system servicing.
Spare partsTrack seals, bearings and kits so critical pumps are covered.
Condition-based triggersCreate work from readings that cross limits you define.
Mistakes that shorten bearing and seal life
- Replacing seals without finding the cause. A new seal in the same conditions fails the same way.
- Over-greasing. More lubricant is not better, and it can raise bearing temperature.
- Measuring at different points each time. Trends become unreliable if locations change.
- Ignoring the flush system. Blocked lines are a frequent root cause of seal damage.
- Running dry or off-curve. Operating outside the design range damages both seals and bearings.
Frequently asked questions
Which pumps need online monitoring?Usually those with high failure consequence, no standby, or difficult access. Others can use route-based checks.
What is the best early sign of a seal problem?A change in leakage pattern, together with flush or temperature changes, is often the first clue.
How often should pump readings be taken?It depends on criticality and failure history. Shorten the interval when a trend appears.
Can I see a pump inspection workflow?A demo can walk through routes and work orders. Schedule a session.
Catch pump bearing and seal problems while repairs are still planned
Bring pump history, inspection readings and work orders together, so every seal and bearing decision has evidence behind it.