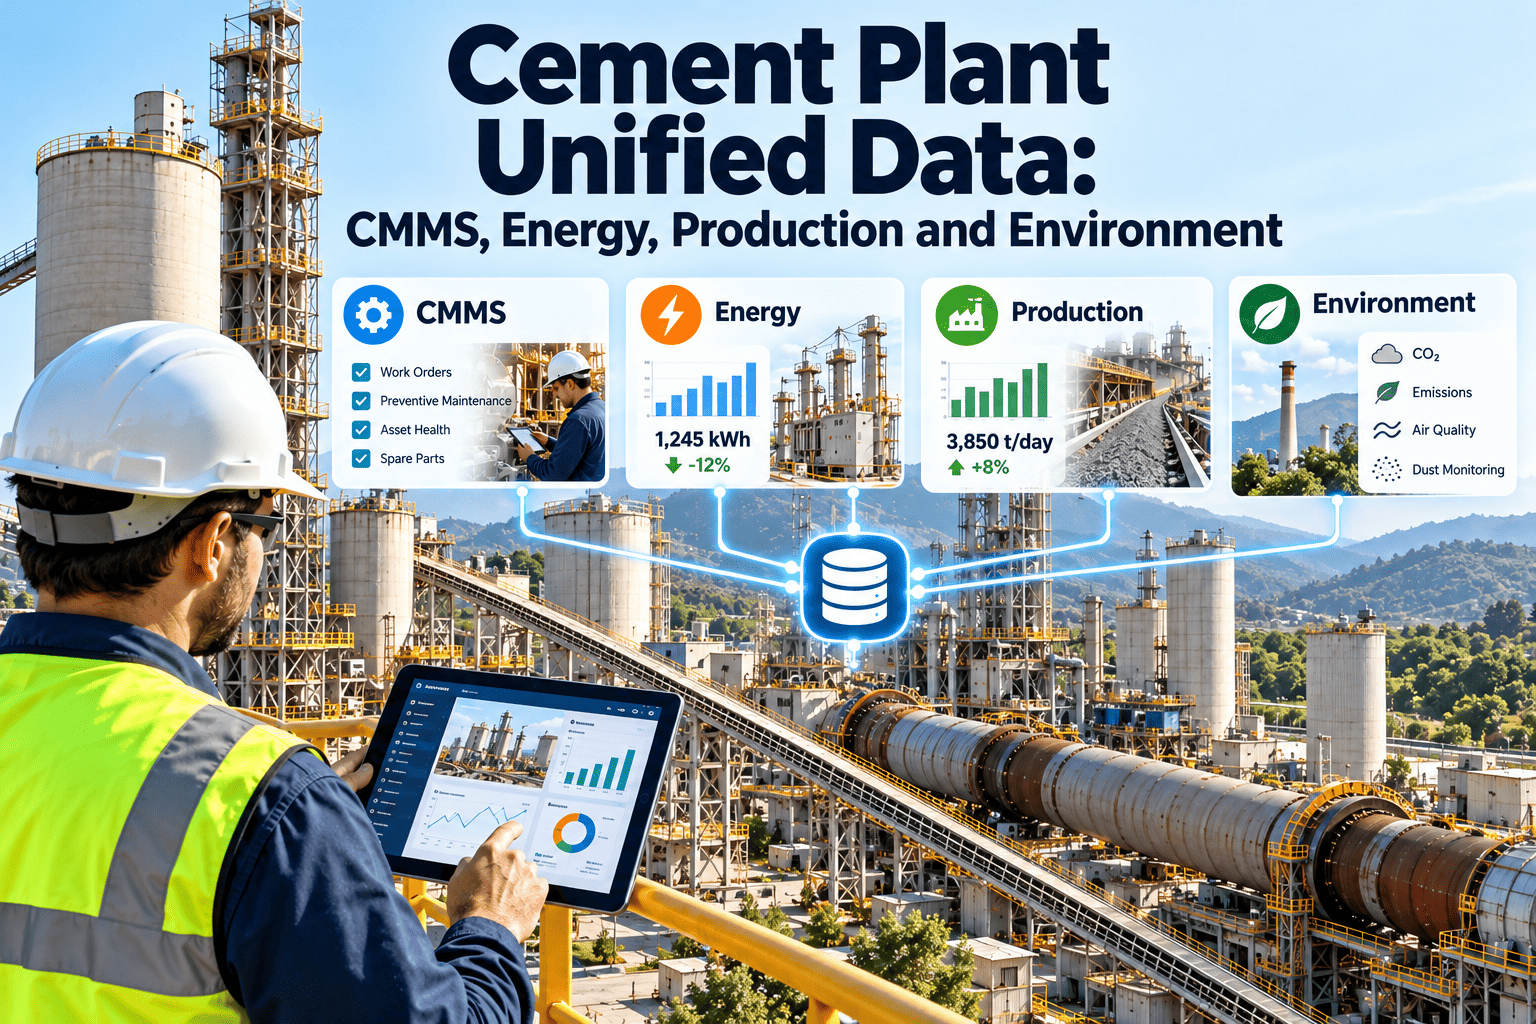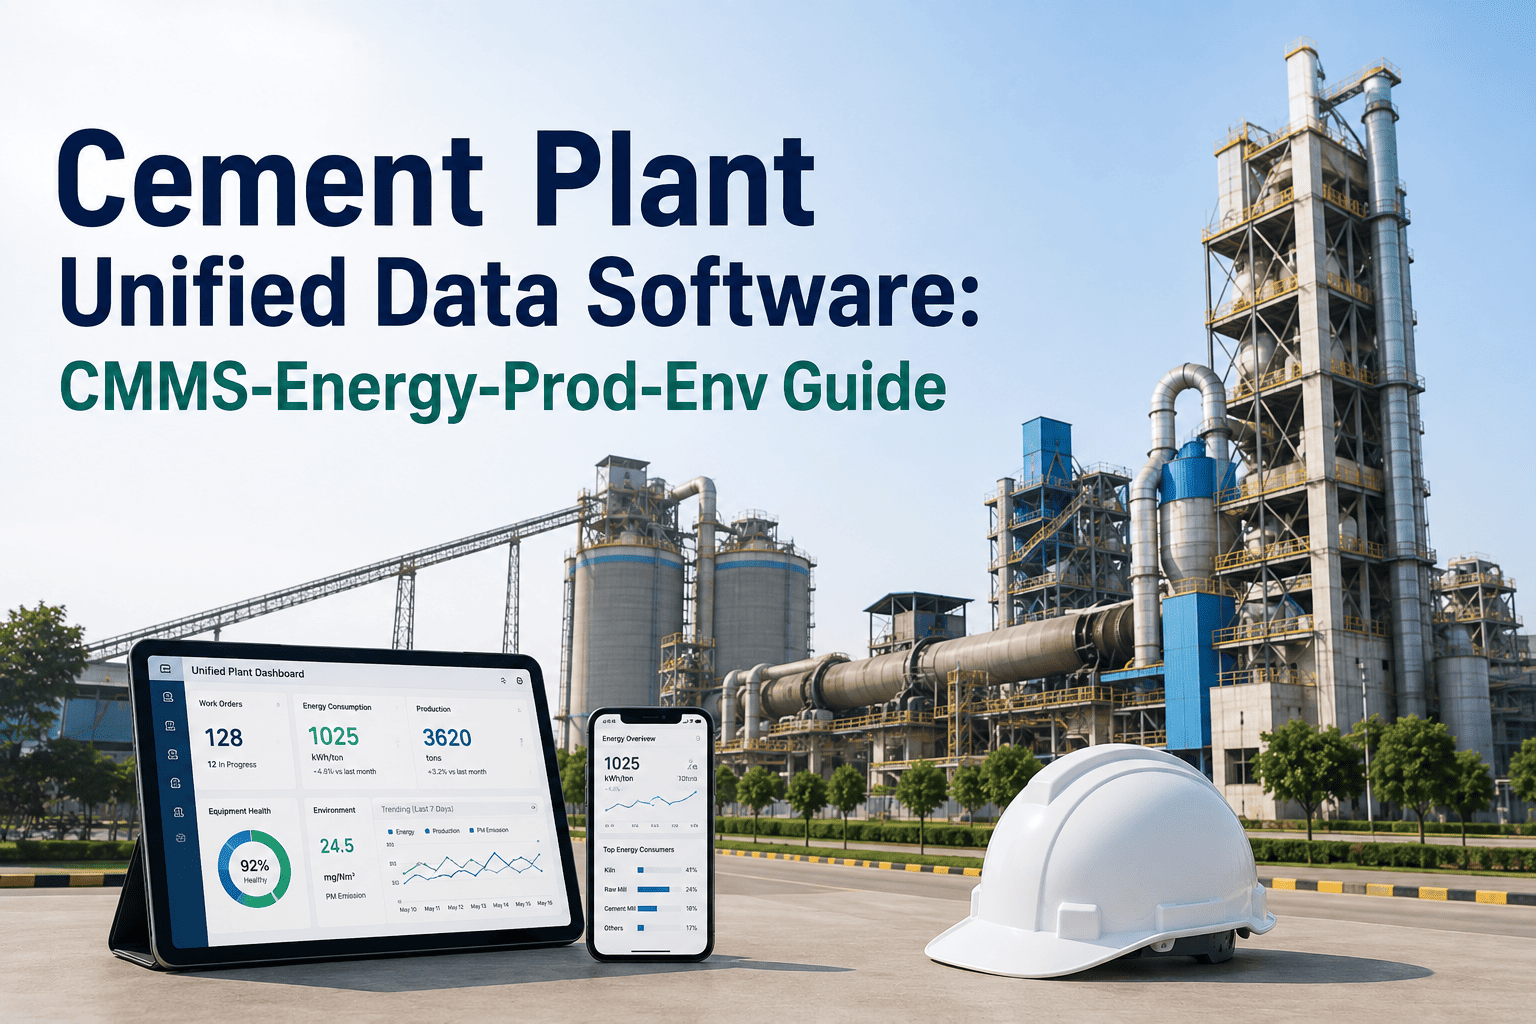
Energy is one of the largest controllable costs in cement manufacturing, and a lot of it is lost to equipment that is slightly out of condition rather than visibly broken. A fan with a worn impeller, a leaking compressed air line, false air at a kiln seal or a separator out of adjustment can each raise specific energy consumption for weeks before anyone links it to maintenance. Energy teams watch kilowatt-hours and fuel; maintenance teams watch work orders. Joining the two shows where energy is leaking. This guide explains how, using Oxmaint maintenance management software for the maintenance side.
Integrating Energy KPIs With Maintenance Data in Cement Plants
Connect specific energy, fan and mill performance to equipment condition and work history, so energy drift triggers the right maintenance action and savings can be checked afterwards.
Why Energy and Maintenance Data Stay Apart
Energy KPIs Worth Linking to Equipment
| Energy KPI | Typical expression | Equipment most involved | Maintenance link |
|---|---|---|---|
| Thermal energy per unit of clinker | Fuel energy per tonne of clinker | Kiln, preheater, cooler, burner | False air, refractory condition, cooler faults, seal wear |
| Raw grinding specific power | kWh per tonne of raw meal | Raw mill, separator, mill fan, drive | Roller and table wear, liner condition, separator settings, fan efficiency |
| Cement grinding specific power | kWh per tonne of cement | Cement mill, separator, fans, conveyors | Grinding media and liner wear, separator efficiency, ventilation |
| Kiln and process fan power | kWh per tonne of clinker, or power at given flow | ID fan, cooler fans, mill fans | Impeller wear, build-up, damper condition, bearing and coupling health |
| Compressed air energy | kWh per unit of air, or load profile in idle periods | Compressors, dryers, distribution lines | Leak repair, filter and drain condition, control settings |
| Auxiliary and conveying power | kWh per tonne moved | Conveyors, elevators, feeders | Misalignment, idler seizure, chain and belt condition |
| Electrical power quality | Power factor and losses | Motors, transformers, drives | Motor condition, connections, capacitor bank and transformer checks |
How Equipment Condition Shows Up as Energy Loss
| Condition | What energy data may show | How to confirm | Typical corrective action |
|---|---|---|---|
| Worn or fouled fan impeller | More power for the same flow, or lower flow at the same power | Inspection, vibration check, performance comparison with baseline | Clean, repair or replace the impeller, then rebalance |
| False air at kiln or preheater seals | Higher fan load and extra fuel per tonne | Oxygen readings, seal and expansion joint inspection | Replace seals, repair joints and inspection doors |
| Worn mill liners or grinding elements | Higher kWh per tonne at the same fineness | Mill inspection, wear measurement, product fineness records | Schedule replacement or recharge based on measured wear |
| Separator out of condition | More recirculating load and mill power | Separator inspection, product fineness, circulating load data | Adjust or repair internals, check seals and drive |
| Compressed air leaks | Compressor load during non-production periods | Ultrasonic leak survey, night-time load profile | Repair leaks, fix drains, review pressure setpoints |
| Misalignment and poor lubrication | Higher motor current and bearing temperature | Alignment check, vibration and temperature trends | Realign, correct lubrication, replace worn components |
| Clogged filters and dust collectors | Higher differential pressure and fan power | Pressure drop trend, bag and cleaning system inspection | Replace bags, repair cleaning system, clear blockages |
From Energy Drift to Maintenance Action
Find the Energy Hiding in Your Maintenance Backlog
Link equipment condition, work history and energy performance in one place, then prioritise the jobs that return the most.
Prioritising Energy-Related Work
Making the Data Line Up
What to align
- Meter and sub-meter points mapped to asset IDs in the maintenance system
- Shared timestamps and shift calendars across energy, process and maintenance records
- Operating mode flags, such as running, idle, start-up and stopped
- Product type and throughput alongside each energy reading
- Work order dates that reflect repair completion, not late closure
What to avoid
- Comparing energy values across different product grades or fuel mixes without adjustment
- Claiming savings from a single before-and-after reading
- Treating metered area totals as proof of one machine's condition
- Ignoring planned stops and start-ups, which distort the averages
- Leaving the energy benefit out of the work order, so no one can check it later
Energy-Aware Tasks for Preventive Maintenance
- Check impeller wear and build-up
- Verify damper and inlet vane position
- Inspect couplings and alignment
- Record motor current at a known load
- Measure liner and roller wear
- Check separator internals and seals
- Review grinding media condition
- Compare fineness and power records
- Inspect seals and expansion joints
- Look for shell hot spots
- Check cooler fans and grate condition
- Review oxygen and draught readings
- Run periodic air leak surveys
- Check dryers, filters and drains
- Review compressor load profiles
- Inspect insulation on hot lines
KPIs That Show Whether the Link Is Working
Where Oxmaint Fits
- Energy meter and process historian data usually stay in their own systems, so decide early how those values will be brought into reviews, whether by shared reports or an agreed data feed.
Building a Baseline You Can Trust
- Review baselines after any major equipment change, because a new impeller or liner set creates a new reference point.
- Keep the baseline method documented, so another engineer can reproduce the same comparison months later.
- Store the baseline against the asset record itself, along with the date, operating mode and the conditions it was captured under, so anyone reviewing a later deviation can see what it is being compared with.
- Where a meter covers several machines, use motor current, run hours or short isolation tests to apportion consumption, and note the method as an estimate rather than a measurement.
An Illustrative Scenario: Rising Fan Power
The sequence below is a hypothetical example, not data from a specific plant, showing how joined-up data shortens the path from signal to fix.
A Staged Approach
Common Pitfalls in Energy and Maintenance Integration
- Chasing every kilowatt-hour: focus on the large consumers first, because small loads rarely justify the effort of data mapping and tracking.
- Blaming equipment for process effects: a change in raw material or kiln stability can move specific energy without any change in machine condition, so involve process engineers in the review.
- Counting savings twice: if a repair and a process adjustment happen together, agree how the benefit is attributed before reporting it.
- Letting energy findings sit in a spreadsheet: without a work order and an owner, an observation about energy loss rarely turns into a repair.
- Forgetting safety and quality: an energy-saving change to a setpoint or a deferred repair must not weaken safety, emissions control or product quality, so the usual approvals still apply.
- Ignoring the people: operators and technicians often notice leaks, noise and odd readings first, and a simple way to log these observations produces useful early signals.
Reporting Energy and Maintenance Results Together
- Start with exceptions: list the circuits where normalised energy has drifted, with the open work and recent findings next to each one.
- Show the link to cost: pair energy deviations with repair cost and downtime risk, so a leak repair and a mill shutdown can be compared fairly.
- Separate verified from estimated: label savings that were confirmed after a repair differently from estimates used to justify a job.
- Keep the audience in mind: operators need circuit-level signals, planners need ranked work, and management needs a short summary of results and open risks.
- Review the method yearly: check whether baselines, tolerances and KPI definitions still reflect how the plant runs, and update them with a note of the change.
Frequently Asked Questions
Treat Energy Drift as a Maintenance Signal
Connect energy KPIs with equipment condition and repair history, and turn quiet losses into planned, verified work.